The Importance of a Robust Quality Management System (QMS) at AMT

AMT – Delivering Excellence in Medical Clean Room Assembly Across Singapore

Nearly 70% of medical device contamination stems from assembly or transport. This underscores the critical role that cleanroom assembly plays in ensuring both patient safety and securing product approvals.

With over three decades of experience in AMT’s medical clean room assembly, AMT Medical Clean Room Assembly Services is a key player in Singapore. They have about 350 employees and provide services to over 30 countries. This makes Singapore as a central place for medical clean room construction and precise assembly work.

Key certifications for AMT include ISO 13485, ISO 9001, and IATF 16949. They adhere to strict quality systems to help with regulated device programs. Their facilities include support for Class 100K (ISO Class 8) clean rooms. They also offer services like single-site injection molding, tooling, and assembly. This reduces the risk of contamination and simplifies the process.

This article covers how AMT’s services for medical clean room assembly help with meeting regulatory requirements. Furthermore, it details their methods for managing microbial control and integrating various processes. These efforts assist medical manufacturers accelerate their product market launch. They also serve to protect the sterility of products and safeguard intellectual property.

Overview of AMT Medical Clean Room Assembly Services

AMT Pte. Ltd. is based in Singapore and has been a trusted partner in medical device manufacturing for over 30 years. They work with clients from more than 30 countries and have solid ties with suppliers in Asia. Around 350 local employees work at the Singapore headquarters to provide regional support.

AMT is renowned for its high-quality standards, thanks to key certifications. Compliance with medical device regulations is assured by their ISO 13485 certification. ISO 9001 guarantees quality management across all operations. IATF 16949 shows their capability in automotive-grade process control, useful for medical device assembly.
medical clean room assembly by AMT

One of AMT’s primary strengths is its single-site integration. Everything from tooling and 3D metal printing to metal and ceramic injection molding and clean room assembly is managed in one place. This approach reduces lead times and minimizes the risk of contamination.

Both sterile and non-sterile products can be handled by AMT’s clean room assembly services. Their integrated workflows for molding, inspection, packaging, and assembly improve traceability and quality control. This makes production more efficient.

AMT’s vertical integration model is a major advantage for clients needing assembly in controlled environments. Having tooling and molding close to cleanroom operations reduces the number of handling steps. This also simplifies logistical challenges and guarantees consistent control over the environment.

AMT – medical clean room assembly

Medical clean room assembly services are offered by AMT. These offerings are designed to help medical device manufacturers located in Singapore and the surrounding regions. Their focus is on clean production within areas classified as ISO Class 8. Here, parts are produced, put together, and packed with strict cleanliness rules. Comprehensive services for molding, assembly, validation, and microbial testing are provided by AMT.

Key Services and Definition offered under this keyword

Medical clean room assembly is a specialty of AMT. This activity takes place in cleanrooms specifically designed for medical device components. The main services are molding in cleanrooms, putting parts together, final packing, checking the environment, and testing for microbes. AMT contributes to the production of surgical parts and devices that demand a sterile environment.

How Class 100K (ISO Class 8) cleanrooms support device manufacturing

The air in Class 100K cleanrooms is maintained at a level of cleanliness suitable for a wide range of assembly tasks. This is effective in preventing particle contamination for devices such as endoscope components. Regular checks of the air, differential pressure, humidity, and temperature are conducted by AMT. This practice ensures they remain compliant and maintain thorough documentation.

Advantages of Vertical Integration in Controlling Contamination and Logistics

Contamination is more easily avoided when molding and assembly are co-located. It makes for shorter lead times and simpler quality checks. The method used by AMT minimizes problems, improves traceability, and leads to cost savings from reduced transportation.

This way of working helps keep AMT’s production processes clean and focused. It makes for better products and easier paperwork for manufacturers. They rely on AMT to meet their requirements.

Cleanroom classifications and compliance for medical device assembly

Understanding cleanroom classes helps to match the right environment to product risks. Cleanroom assembly compliance relies on setting clear particle limits, doing regular checks, and having proof of validation. This section delves into the standards for ISO Class 8. It also covers monitoring methods that keep medical assembly lines up to par in Singapore and other places.

Requirements for ISO Class 8

The maximum allowable concentration of airborne particles, categorized by size, is defined by ISO Class 8 cleanroom standards. They are perfect for many medical device assembly jobs where total sterility isn’t needed. The industry often calls it Class 100K. This designation is commonly used for tasks involving plastic injection molding and assembly.

Validation and monitoring practices

Regular checks on the environment are critical for medical cleanrooms. To ensure air particle levels remain within predefined limits, facilities monitor them closely.

To maintain proper airflow, teams monitor the differential pressure between different zones. Temperature and humidity are also controlled to prevent product damage and minimize contamination risks.

Regular validations are performed, and detailed records are kept to prove compliance with regulations. Dedicated teams conduct microbial checks to detect potential issues early on and implement corrective actions as needed.

Regulatory alignment

It is crucial to adhere to regulations established by authorities such as the US Food and Drug Administration and the European Medicines Agency. For device manufacturers, maintaining ISO 13485 certification and comprehensive validation records is key to passing audits and completing regulatory submissions.

Maintaining thorough records of cleanroom procedures, doing requalifications periodically, and tracking data proves manufacturers have everything under control during inspections. Building medical cleanrooms to these standards makes passing regulatory checks easier and speeds up time to market.

Integrated manufacturing: injection molding and clean room assembly

Integrating both molding and assembly in one place makes producing medical equipment more efficient. It means less moving around inside the facility. Plus, it makes it easier to keep an eye on quality, from the molding to the final packaged product.

Advantages of single-site integration

The handling of parts is substantially minimized when injection molding and assembly operations are performed together. This results in faster development of prototypes and a quicker production startup. It allows the tooling, molding, and assembly teams to work closely. This guarantees that quality checks consistently adhere to the same high benchmarks.

Reduction of contamination risk and logistical cost savings

By not moving things between locations, there’s less chance for things to get contaminated. There is also a reduction in costs associated with packaging, shipping, and handling. Centralizing all operations simplifies the management of quality control and regulatory compliance. This contributes to a more efficient clean room assembly process.

Examples of product types suited to integrated processes

This integrated system is well-suited for products such as endoscopic components, surgical instrument housings, and parts for minimally invasive devices. Both sterile and non-sterile products can be manufactured, depending on the specific sterilization and packaging requirements.

Type of Product Main Benefit of Integration Common Control Measures
Endoscopic lenses and housings Reduced particulate transfer between molding and optics assembly ISO-classified assembly areas, particle counts, validated cleaning procedures
Housings for surgical instruments Better dimensional control and batch traceability Material lot tracking, in-line inspection, sterilization validation
Minimally invasive device components Efficient change control for fast design updates Controlled environment molding, bioburden testing, process documentation
Disposable diagnostic housings Lower logistics cost and faster time-to-market Consolidated supply chain, final inspections, batch records

Choosing a facility that handles both clean room assembly and cleanroom injection molding means better quality control and reliable schedules for making medical equipment. This approach reduces risks and preserves value, from the first prototype to the final product shipment.

Use Cases and Environment Choices for Medical Device Assembly

It is essential to select the appropriate environment for medical device assembly. Options available from AMT range from stringent ISO-classified rooms to controlled white rooms. This flexibility helps match the assembly process with the device’s risk level.

Choosing Between a Cleanroom and a White Room for Assembly

Use an ISO-classified cleanroom when specific cleanliness levels are needed. This applies to devices such as implants and sterile disposable products. In cleanrooms, these items are protected throughout the assembly and packaging stages.

Choose white room assembly if higher particle counts are acceptable. It continues to offer controlled conditions, including managed air flow and filtered HVAC systems. This option maintains quality and reduces costs for many devices used outside the body.

Device risk profiles that require ISO-classified environments

Certain devices need sterile assembly environments. Implants and surgical instruments serve as examples. These are typically assembled in sterile, clean environments.

If a device impacts health or its performance can be affected by particles, use ISO-classified spaces. AMT’s cleanrooms offer validated controls for high-risk product assembly.

Lower-risk assemblies suitable for standard controlled environments

Standard environments are well-suited for devices intended for external use or components that will be sterilized later. They are cost-effective and adhere to good manufacturing practices.

Assembly in non-ISO environments helps launch low-risk products faster. It delivers quality without incurring the high costs associated with stringent cleanroom standards.

Assembly Setting Common Applications Primary Control Measures Impact on Cost
Cleanroom (ISO-classified) Implants, sterile disposables, invasive instruments Particle counts, HEPA filtration, gowning, validated procedures High
White room assembly External-use devices, components for later sterilization Filtered HVAC, hygiene protocols, controlled access Moderate
Standard controlled environment Non-sterile subassemblies, prototypes, parts with low risk Basic controls for contamination, cleaning schedules, traceability measures Minimal

Ensuring Quality and Microbiological Control in Clean Room Assembly

Robust quality systems ensure medical equipment is safe and reliable. AMT follows clean room standards. These standards comply with ISO 13485 and the particular requirements of Singapore. Maintaining detailed records and performing regular checks are essential for complying with clean room regulations at every stage of manufacturing.

Schedules for Validation and Documentation Practices

Validation is planned and covers checking the environment, equipment, and processes. This encompasses particle and microbe counting, differential pressure logging, and temperature and humidity tracking. Also, CAPA traces are recorded. All of this documentation helps to prove compliance with the stringent clean room regulations for medical equipment.

Teams and Routines for Microbiological Inspection

Special teams focus on checking surfaces and air, and analyzing cultures. They identify trends, look into anomalies, and verify the effectiveness of cleaning procedures. Their job is to keep strict control over microbes. This assists in preventing contamination of sterile and sensitive medical instruments.

Traceability, batch records, and packaging controls

Detailed records are maintained for every medical device. This includes info on materials, machine settings, and who operated the machines. When it comes to packaging, there are different steps based on the device’s risk. Special sterile packaging is used for sterile devices. Non-sterile items receive protective, non-sterile packaging. Every step ensures proper execution from the start until the final shipment.

Quality Element Common Activities Deliverables
Schedule for Validation Periodic qualification runs, revalidation after change control, seasonal environmental checks Validation protocols, acceptance reports, requalification certificates
Monitoring of the Environment Sampling of air and surfaces, counting particles, monitoring differential pressure Logs kept daily, charts showing weekly trends, reports on exceptions
Microbiology oversight Testing of cultures, investigations of rapid alerts, studies on cleaning effectiveness Microbial test results, corrective actions, method validations
Product Traceability Tracking of material lots, records of operators and equipment, histories of digital batches Full batch records, lists of serialized lots, trails for auditing
Packaging control Validated sterile packaging runs, sealing integrity checks, labeling verification Reports on packaging validation, documentation for sterility assurance, records of shipments

Supporting Technical Capabilities for Medical Equipment Manufacturing

In Singapore, AMT combines precise component technology with cleanroom assembly for manufacturing medical equipment. These capabilities enable design teams to move quickly from concept to an approved product. This happens without waiting long for different companies.

Detailed features that are not possible with plastics can be created using metal and ceramic injection molding. Stainless steel and cobalt-chrome parts are made for tools and implants. Ceramics make parts for checking health and replacing body parts that last a long time and are safe for the body.

In-house tool creation ensures that molds and dies have precise dimensions and surface finishes. Rapid tool modifications significantly cut down on waiting times and lower the risk associated with parts that require a perfect fit. It also keeps costs down when making more for sale.

The process of creating samples is accelerated with 3D metal printing, which also permits the creation of complex geometries. This method allows engineers to verify the form, function, and fit before committing to mass production. Mixing 3D printing with usual molding accelerates the launch of new medical products.

These methods allow for joining different materials like metal, ceramic, and plastic. Joining techniques like overmolding are done in clean spaces to keep everything precise. This leads to dependable combinations for surgery tools, diagnostic setups, and parts to place inside the body.

Using metal and ceramic injection molding, making tools, and 3D printing lets makers have one ally. This ally helps in making samples, approving, and making more advanced medical devices. It cuts down on dealing with many groups, keeps ideas safe, and makes getting official approval smoother.

Advantages in Supply Chain and IP Protection for Contract Manufacturing

The Singapore hub of AMT tightly integrates sourcing, production, and distribution. This supports making medical equipment on a large scale. Centralized workflows are designed to reduce lead times and facilitate planning for large volume orders. For companies that require reliable components and consistent timelines, this approach offers distinct supply chain advantages.

Strong partnerships in Asia ensure steady materials and cost management. Trusted vendors in Malaysia, Thailand, and Vietnam are among AMT’s collaborators. This secures the materials, parts, and logistics needed. Such a network simplifies shipping and ensures timely deliveries for urgent projects.

AMT takes serious steps to protect clients’ intellectual property during contract manufacturing. The use of confidentiality agreements and controlled access to engineering files are standard practices. Segmented production lines also help keep client designs and processes safe. These measures comply with the stringent standards of regulated industries, which ensures the security of tooling and prototype development.

Processes that are ready for audit and a skilled workforce assist in protecting intellectual property and meeting regulatory demands. A traceable record is created by documenting design transfers, modifications, and supplier information. This reduces risks when moving from prototype to mass production in a medical clean room.

Designed for scalability, the Singapore platform serves customers across more than 30 countries. This arrangement enables AMT to ramp up production without adding complexity to its processes. So, companies can smoothly go from small test runs to making large quantities of surgical tools and diagnostic devices.

Predictable planning and various options for regional transportation are benefits for customers. This expedites market access. For medical equipment companies, working with a partner who manages local logistics and IP security is smart. It offers an effective way to distribute globally while protecting unique tech.

Operational efficiency and cost considerations for clean room projects

Overseeing clean room projects focuses on budget and timeline drivers. The costs of clean room assembly are weighed against the benefits in quality and speed by the teams. The approach taken by AMT in Singapore exemplifies how expenses can be managed while adhering to standards.

Costs depend on cleanroom level, validation extent, and monitoring intensity. High levels require better HVAC and filtration, leading to higher initial and ongoing costs.

The costs are increased by validation and monitoring due to the required tests and documentation. These are critical for meeting standards from bodies like the US FDA. Planning is required for the costs associated with requalification and continuous data collection.

Expenses are reduced by integrating manufacturing processes. This minimizes transportation needs and the requirement for multiple validations. This approach often saves money in medical device assembly.

Working with a full-service clean room partner can shorten project times. This leads to better coordination and traceability, which in turn reduces the total costs.

There are trade-offs involved in selecting the appropriate quality level. High-risk devices need more controlled environments. Less demanding conditions are suitable and more economical for simpler components.

Strong quality systems, such as ISO 13485, are the source of efficiency. Early regulatory alignment assists innovation while focusing on production readiness and validation.

To decide on a production setting, weigh all costs and rework risks. This balanced perspective helps to ensure that projects meet the required standards while also being cost-effective.

Customer industries and product examples served by AMT

In Singapore and other Asian regions, AMT serves a wide range of medical clients. They make parts for hospitals, device OEMs, and labs. Their services cover everything from single prototypes to large-scale production runs for medical equipment.

Below are some examples of how AMT supports specific products and industries. They connect manufacturing skills with the needs for quality and use.

Surgical and endoscopic components and assemblies

AMT makes things like optics housings and grip modules for surgery. Assembly is conducted in cleanrooms to prevent particulate contamination. This production process adheres to strict standards for dimensions, surface finish, and clinical application.

Medical consumables and diagnostic components

They make disposable items like syringe parts and test cartridge houses. AMT combines clean assembly and tracking systems to meet rules. Diagnostic parts they make include sample ports and holders for tests.

Parts for Implantation and High-Precision Applications

AMT supports making implantable parts with special materials and methods. They use metal and ceramic molding for these parts. Strict checks are in place for safety records and manufacturing history.

Case examples, patents, and awards

AMT has 29 patents in 12 countries and 15 inventions. These support their unique tools, metal processes, and assembly setups. The awards they have received in metalworking showcase the skills that contribute to the manufacturing of medical devices.

Product Type Typical Processes Primary Quality Focus Typical End Market
Endoscopic toolheads Injection molding, cleanroom assembly, ultrasonic welding Precision in dimensions, low generation of particulates Hospitals for surgery, centers for ambulatory care
Single-use consumables Manufacturing of medical consumables, automated molding, packaging Traceability, sterility assurance for sterile items Clinical labs, emergency care
Diagnostic cartridges Assembly of chambers for reagents, micro-molding, testing for leaks Fluid integrity, lot-to-lot consistency Point-of-care diagnostics, centralized labs
Components for Implantation Finishing, metal injection molding, validated procedures for cleaning Biocompatibility, manufacturing history files Dental, orthopedics, cardiovascular fields
Precision Parts (MIM/CIM) Heat treatment, powder metallurgy, machining (secondary) Reliability in mechanics, properties of materials Assembly of medical devices – %anchor3%, manufacturers of instruments

Conclusion

AMT’s work in Singapore demonstrates high-quality medical device assembly in clean rooms. They are certified with ISO 13485, ISO 9001, and IATF 16949. They also have Class 100K cleanrooms. This capability allows AMT to safely manage complex diagnostic tools, surgical components, and implants.

In their approach, multiple processes are combined at a single location. This includes on-site capabilities for injection molding, tooling, MIM/CIM, and 3D metal printing. The risk of contamination is lowered, and transportation times are reduced as a result. This method ensures safe medical device assembly in Singapore. Furthermore, it safeguards intellectual property and improves collaboration with suppliers throughout Asia.

Strong quality assurance and various options for microbiological control are offered by AMT. Teams can choose cleanroom classes based on the risk of the device. This approach creates a balance between cost, regulatory compliance, and time to market. AMT’s medical clean room assembly represents a wise choice for companies in search of a dependable partner. It promises scalable, reliable production in Asia.
How Local Codes Affect Valve Choices

Cast Iron Gate Valves: Key Features, Advantages, and Applications

Might one quality valve shrink maintenance time and keep water networks running longer?

I produce and stock Cast Iron Gate Valve Manufacturer at Yaxing Valve, and I stand behind their quality and service for U.S. customers. This line is engineered for longevity in public water and light industrial applications.

Every valve combines a rugged cast-iron body, a precision-machined wedge guide, and simple handwheel operation. That means reliable shutoff, easy upkeep, and predictable performance in mechanical rooms, fire loops, and distribution networks.

I support specifiers with fast submittals and transparent details: sizes, connection types, pressure classes, and optional accessories. My site stores account preferences and carts via cookies to simplify repeat orders.

When you want a practical replacement or budget-smart choice for new work, compare these cast-iron gate valve advantages against your current hardware to see lifecycle value and real-world fit.

Why I Trust Yaxing Valve Cast Iron Gate Valves for Reliable Flow Control

I personally review each product at Yaxing Valve, allowing confident recommendations for tough U.S. sites.

Built for industrial performance with a robust cast iron body

I build every unit with a robust cast iron body that resists deformation under load. Precision machining with metal-to-metal seating provides tight shutoff at critical moments.

Cast Iron Gate Valve Manufacturer

Designed to maximize flow with minimal pressure drop

The internal path is optimized to lower turbulence and pressure loss. This helps pumps operate efficiently while reducing energy consumption.

  • Dimensions and testing are validated to ANSI norms and internal criteria.
  • I refine stem/wedge/bonnet interfaces to reduce friction and maintain consistent torque over time.
  • I set body thickness targets for durability while keeping weight manageable for installers.
  • Documentation lists tests/standards so purchasing can wrap orders quickly.
Key Feature Primary Benefit Specification
Cast iron body High rigidity Meets dimensional stability targets
Streamlined gate Reduced pressure drop Improves pump efficiency
Refined stem and handwheel Smoother operation Stable torque for extended life
Spec documentation Speedier submittal clearance Reports aligned to ANSI

Cast Iron Gate Valves—Materials, Design Details, and Key Performance

I break down body, sealing, and stem options to simplify selection and ordering.

Materials: body, bonnet, and wedge

The material stack includes a cast-iron body/bonnet, a precision-machined wedge, and metal-to-metal seating for dependable isolation across water service and general industry.

Stem/Handwheel configurations

For compact layouts, I offer non-rising and inside-screw stem options. Each screw thread form and packing arrangement is documented in my product details.

Performance Envelope and Standards

I publish qualified pressure and temperature ranges and align end connections to common ANSI standards to help engineers confirm fit without additional drawings.

  • Stem/handwheel interface tuned for steady torque.
  • Optimized internals minimize pressure loss through the gate.
  • Clear series IDs and submittal specs accelerate approvals.
Component Material/Type Rating Notes
Body & Bonnet Cast iron Class 125/approx. 150 psi ANSI flange sizing; weld/bolt options
Valve wedge Precision-machined metal −20°–180°F range Metal seat with low-loss finish
Operating stem Inside-screw / non-rising N/A Documented thread and packing in datasheet
Model series Series YX-100, YX-200 2″ to 12″ sizes Part numbers simplify bidding

Modern Applications, Install, and Operation

I advise contractors/owners on best-fit placements in today’s water and utility circuits. The goal is straightforward selection, installation, and checks so crews complete commissioning without callbacks.

Waterworks, building systems, and general industry applications

Choose full-bore units when low restriction is critical—long mains, service feeds, and bypasses gain the most.

For mechanical rooms and industrial loops with limited headroom, I favor non-rising stem or inside-screw designs.

Install best practices

Protect the valve body during handling; lift at rated points and avoid flange stress. Confirm alignment prior to final torque to prevent distortion/leaks.

Pick gaskets compatible with your media, follow a cross-torque sequence, and set support spacing to avoid pipeline sag.

Operation and maintenance notes

Set the handwheel for comfortable access and verify free stem/handwheel movement after packing adjustments.

Perform periodic torque checks under pressure, inspect the wedge and packing, and confirm the pressure/temperature range against your media. Record tag numbers in your maintenance account and link CMMS work orders.

Topic Action Phase Result
Application mapping Use full-bore on mains; inside-screw/NRS in tight spots Planning Less pressure loss and space efficiency
Handling/installation Lift properly, align, then cross-torque bolts Install Avoids stress-related leaks
Operating checks Confirm handwheel feel; perform pressure tests Commissioning and routine Consistent operation and shutoff
Maintenance tracking Tag units and connect to CMMS/account Ongoing cycle Faster parts tracking and replacements

Good handling and careful commissioning prolong service life and keep Resilient Seated Gate Valve in top shape.

Specify the Right Iron Gate Valve with Me at Yaxing Valve

Contact me with your line size, pressure expectations, and flow needs and I will match the exact series and type to your duty range and temperature limits.

A short checklist helps submittals pass first review: ends, inside-screw or non-rising choice, handwheel orientation. I also capture stem/handwheel and screw details for clear install guidance.

View the images gallery for high-resolution images and a clean gallery layout that shows clearance and operator reach. Make an account to save specs, tag valves, and link drawings plus a one-page field PDF.

Reach out for a quick quote; I’ll confirm stock/lead times, suggest series alternatives, and help finalize your order as you review the gallery. We only use cookies to keep your session and cart active.

Compact Fiber Unit for Telecom Carriers

FTTH Cable Production: How the Manufacturing Process Works

Quick fact: in excess of 70% of new U.S. broadband builds now rely on fiber networks that demand tight manufacturing control to hit performance targets.

Shanghai Weiye OFC Equipment manages full-cycle SZ stranding line manufacturing, from choosing brand fibers like Fujikura or Corning® SMF-28e to complete test reports that guarantee full quality assurance.

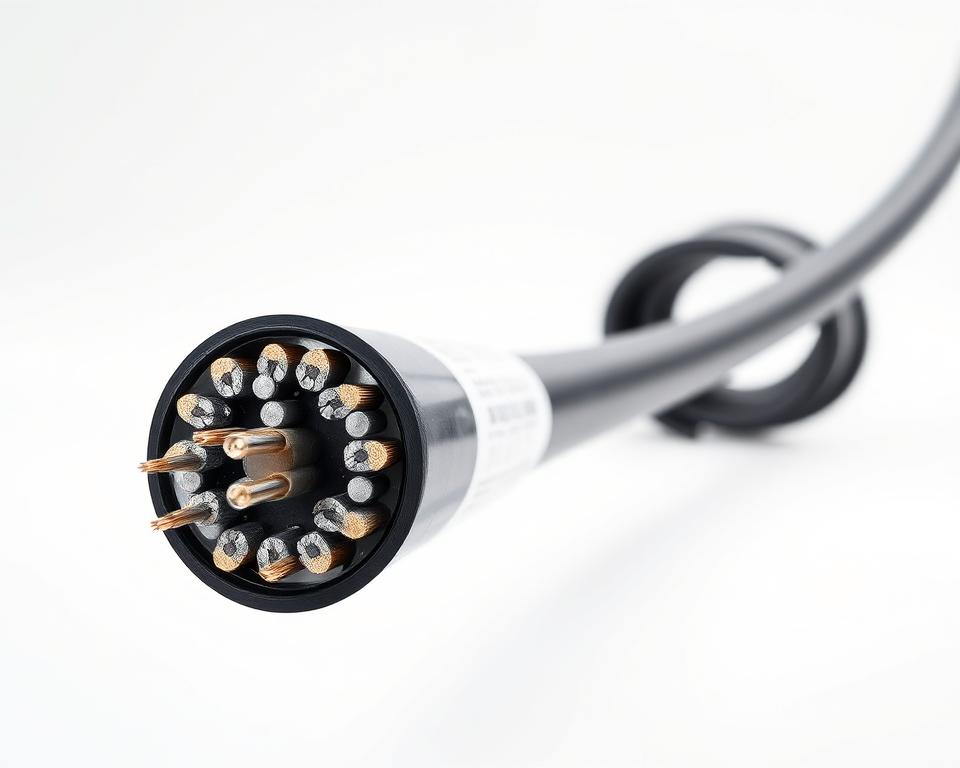
Our drop cable designs are built for overhead, underground, and direct-buried installation, with LSZH, PVC, and polyethylene (PE) jacket options and arrangements from 1–4 cores. We offer single-mode OS1/OS2 and OM2–OM4 grades plus G.652D and ITU-T G.657 variants, Pantone sheath colors, and logo printing.

Automated machines and high-precision equipment stabilize line speed and keep repeatability high. Typical lead times run 4–5 days for orders < 100 km and 7–10 days for < 500 km, with an min. order of 1 km and free-replacement warranty for quality problems.

Read on to understand how materials, testing, and support work together to reduce lifecycle cost and pair the right product with your network.

  • Shanghai Weiye OFC Equipment delivers end-to-end manufacturing and lab testing for United States projects.
  • A range of jacket options and optical grades support indoor/outdoor environments.
  • Automated production lines provide consistent quality and reliable optical performance.
  • Quick lead times, low minimums, and recognized brand fibers support reliable procurement planning.
  • Complete reports and after-sales warranty back product reliability and compliance documentation needs.

Expert FTTH manufacturing by Shanghai Weiye OFC Equipment

When deadlines and performance are critical, Shanghai Weiye OFC Equipment provides customized drop cables with complete test documentation.

As a specialized maker and supplier, Shanghai Weiye OFC Equipment combines purpose-built equipment with tight material control. We offer custom builds and services for residential/MDU deployments. Every order includes 100% quality assurance and complete test reports.

Our lab conducts high heat, salt spray, and vibration tests to verify durability. Jacket options include LSZH, PVC, and PE. Designs cover bow-type flat and self-supporting styles and support brand fibers such as Fujikura® and Corning SMF-28e.

FTTH cable production line

  • Documented line control and in-process checks for auditable shipments.
  • Engineering support for specs, trials, and ramp to volume.
  • Modern fixturing and calibration reduce variability so every cable meets carrier standards.

FTTH Cable Production

At Shanghai Weiye OFC Equipment, manufacturing steps are matched to network specs, combining brand fiber choices with disciplined test flows.

Selecting Optical Fiber and Brands

We match fiber secondary coating line to bend radius, attenuation, and deployment type. Options include OS1, OS2, OM2–OM4 and ITU-T G.652D, G.657.A1/A2. Brand fibers such as Fujikura® and Corning SMF-28e are offered to meet procurement standards.

Strength Member Options

Strength members employ dielectric FRP or metallic steel wire. FRP is ideal where non-conductive runs are required. Steel wire adds tensile strength for longer aerial spans and bonding/grounding needs.

Jacket extrusion and process control

Jacket options include LSZH for indoor flame safety, PVC for flexibility and ease of handling, and PE for UV/moisture resistance outdoors. Closed-loop control of extruder temperature and capstan speed keeps line speed stable and dimensional tolerances.

Member Dielectric FRP Metallic Steel
Use case Electrical isolation Aerial spans, high tensile
Advantage Light, non-corrosive High strength
Installation note Simple terminations Requires grounding

In-Process and Final Testing

Inline geometry and concentricity checks operate in-line. Final optical tests verify attenuation and reflectance. Each order includes a full test report and lab results from high heat, salt fog, and vibration trials to confirm handling for drop terminations and field use.

Typical lead times are under 100 km in 4–5 days and under 500 km in 7–10 days. Lot records and FAI approvals provide traceability and compliance for U.S. programs.

FTTH drop cable types and structures we manufacture

Shanghai Weiye OFC Equipment provides a focused portfolio of FTTH drop designs that fit indoor risers and long aerial runs. Each option pairs tested materials with geometry tuned for field termination and consistent optical performance.

The bow-type flat drop cable minimizes footprint for risers/ducts. It keeps bend loss low for easy routing in hallways and MDUs.

Self-Supporting Aerial Designs

Self-supporting FTTH drop designs include a support messenger to carry tensile loads. Choose dielectric FRP for non-conductive runs or steel messenger when bonding/grounding and extra tensile strength are required.

Core Layouts and Strength Members

We provide both dielectric and metallic strength member configurations to meet safety/EMI requirements. Central loose-tube and unitube flat types balance crush resistance and Fiber coloring machine for quick termination.

Indoor vs Outdoor Jackets

Jacket choices include LSZH for flame-retardant, low-smoke indoor use and PE for outdoor durability. Each family is validated for mechanical/optical performance before shipment.

Design Best use Strength element Sheath
Bow-type flat Indoor risers and MDUs FRP (dielectric) LSZH
Self-supporting Aerial spans Steel wire or FRP Polyethylene
Central loose-tube Higher fiber counts FRP LSZH or PE
Flat unitube Low count, quick strip FRP or steel LSZH or PE

Production line equipment that ensures quality and speed

Automation with sensor feedback at Shanghai Weiye OFC Equipment reduce manual handling and increase throughput for drop patch preparation.

Our production line uses automated machines that cut/strip drop cords to raise throughput and reduce operator variability.

The CLX-BPO2 automated stripper runs under PLC and photoelectric control. One cycle is about 1.5 seconds, giving ~20 terminals per minute in production.

Automated Cut/Strip for Drop Cords

The equipment strips LSZH/PVC jackets and trims FRP or steel strength members to precise stub lengths. Pneumatic cylinder actuators provide quick, repeatable motion and low downtime.

Closed-Loop Control for Repeatability

PLC logic + photoelectric sensors deliver precise positioning and feedback control. Inline checks update SPC charts so operators can correct trends before out-of-control conditions occur.

Feature Capability Result
Machine 1.5s cycle, auto-strip High throughput
Drive Pneumatic cylinders Fast/reliable motion
Materials LSZH/PVC; FRP/steel Clean, accurate preps
Process control PLC + photoelectric + inline checks Consistent quality, lower rework
  • Auto scrap ejection and ergonomic feeders maintain clean workcells.
  • PCPs document calibration and key parameters.
  • Integrated assets and trained operators help meet FTTH volume goals without compromising accuracy.

CLX-BPO2 Capabilities on Our Line

The CLX-BPO2 brings industrial-grade stripping and trimming to our line, reducing cycle time while maintaining consistent prep.

Shanghai Weiye OFC Equipment uses the CLX-BPO2 to increase throughput and standardize terminal quality. The unit runs at an approximate cycle time of 1.5 seconds, producing around 20 preps per minute in production.

PLC and photoelectric control deliver exact detection and repeatable actuation. That control helps keep strip lengths and reserved strength stubs within tight tolerances.

Line Speed

Typical operation speed is 1.5s per cycle. This converts to steady throughput under continuous line conditions.

Supported Strip and Stub Lengths

The CLX-BPO2 strips LSZH and PVC jackets with an adjustable jacket strip length from 17.5 to 35.0 mm. Reserved strength member stubs are set between 7.0 and 11.0 mm to match common termination hardware.

Cutting FRP/Steel Members

The machine cuts FRP/steel strength elements cleanly while protecting adjacent fibers. Custom tooling are available for nonstandard sizes to maintain precision.

  • Automatic waste ejection and sensor start reduce idle time.
  • Small footprint (L40 × W18 × H18 cm), 50W at 110–220V, and 11 kg mass ease integration into workcells.
  • Cylinder-driven motion and PLC/photoelectric control improve line reliability and lower maintenance interruptions.
Spec Rating Benefit
Cycle time ≈1.5 s (~20/min) High throughput for production runs
Strip lengths (A) 17.5 to 35.0 mm Compatible with common connectors
Reserved stub (B) 7.0–11.0 mm Supports termination strength
Power & size 110–220V, 50W; 40×18×18 cm Easy integration into existing equipment

Using this machine, Shanghai Weiye OFC Equipment standardizes prep so field teams receive drop parts ready for quick installation. The CLX-BPO2 supports our lines in meeting volume targets without compromising quality.

Custom Specs for Your FTTH System

Shanghai Weiye OFC Equipment configures every order to meet your network requirements and simplify deployment. We combine focused options with predictable schedules so your teams get install-ready reels.

Choose 1 to 4 cores with SM or MM fiber. Options include OS1/OS2 plus OM2–OM4 along with G.652D/G.657 variants to align with optics and connector plans.

We match sheath colors to Pantone codes for fast field ID and consistent asset tags.

Jackets, Legends & Branding

Select LSZH, PVC, or PE jackets based on route and safety rules. Custom legends/logos support inventory and warranty tracking.

Put-Ups, Packaging, and Structures

Standard put-ups are 1 km, 2 km, and 4 km with custom reels and packaging to fit storage/handling. Choose flat bow-type or self-supporting and FRP or steel members to meet span and isolation needs.

Choice Common choice Advantage
Length 1 / 2 / 4 km Less staging, easier reels
Jacket LSZH, PE, PVC Indoor/outdoor compatibility
Design Flat bow / Self-supporting Flexible routing/span

As a manufacturer, Shanghai Weiye aligns runs to your schedule and provides docs that detail final specs for straightforward QA on site.

Quality assurance, testing, and documentation

Shanghai Weiye OFC Equipment embeds quality checkpoints across the production line so every item has recorded acceptance data at ship.

Lab Testing: Heat, Salt Spray & Vibration

Our lab conducts high-temperature exposure, salt fog corrosion, and vibration tests to qualify materials and assemblies. These tests simulate field stresses for indoor/outdoor applications.

100% test reports for every cable

Every fiber optic cable ships with a 100% test report that records loss, return loss, and key geometry where applicable. Final inspection gates prevent nonconforming shipments before they leave the factory.

Traceability & Compliance

Lot/batch records link tests to reels/serials so audits and warranty claims are simple to verify. Documentation uses standard customer templates to speed approvals and inbound inspection.

  • Line checks and final inspection reduce field failures and cut warranty events.
  • Quality packages include spec confirmation and formatted data for quick review.
  • Ongoing trend analysis inform preventive maintenance and improve long-term reliability.
Trial Why Outcome
High-temperature Thermal stability Validated heat endurance
Salt spray Corrosion resistance Qualified for outdoor use
Mechanical vibration Resistance to vibration Reduced field failures

FTTH Drop Cable Pricing & Cost Drivers

Budgeting for a drop run starts with fiber and jacket choices and is refined by volume and customization.

Typical prices range broadly—from about $30–$1,000 per unit—based on fiber grade, jacket chemistry (LSZH, PVC, PE), length, and design structure.

Material choices, fiber grade, jacket type, and structure

The primary cost drivers are fiber grade, sheath material, and the structural type chosen for deployment.

Self-supporting structures and steel members increase material/labor. Custom colors, logos, and print legends add setup time and influence price for short runs.

Length/Volume/Customization Impact

Longer reels and higher volume orders reduce unit cost. Short runs often carry setup fees and higher per-unit charges.

  • Changeovers and special cutters increase lead time and add cost.
  • Clear RFQs and line scheduling let Shanghai Weiye OFC Equipment match quotes to delivery windows.
  • Frameworks and indexed pricing stabilize budgets over phases.
Factor Effect on price Guidance
Optical grade High impact Right-size spec to budget
Jacket type Medium Compare LSZH vs. PE for total cost
Order length / volume High impact Consolidate where possible

Logistics for the U.S.

Shanghai Weiye OFC Equipment makes lead times and logistics clear so planners can align staffing and sites. Predictable windows reduce downtime and control costs when a rollout is underway.

Typical production windows and capacity planning

Typical production windows are 4–5 days for < 100 km and 7–10 days for < 500 km. We schedule line capacity to match your rollout milestones and to maintain on-time delivery.

The service team issues production updates and tracking so installation teams can plan arrivals. For compressed schedules, we reserve contingency capacity to pull in critical-path orders.

Why MOQ Matters

The MOQ is 1 km. This reflects line setup such as wire/die adjustments that consume start-up material and scrap.

We review your put-ups and staging to choose reel sizes that cut waste and handling. Batch releases can balance inventory with more frequent small-site deliveries.

Installation Scenarios & Readiness

Site conditions dictate whether a self-supporting span, duct pull, or direct-buried run is the best fit for a project.

Deployment Considerations

For aerial runs, Shanghai Weiye OFC Equipment advises self-supporting designs with correct strength members to manage sag/tension for long-term stability.

Duct installations work best with low-friction jackets and crush-resistant builds so pulling avoids fiber damage. PE jackets are typical for underground and buried paths where moisture resistance matters.

Direct-buried designs require proper depth control per local codes and moisture barriers to protect the fiber core long-term.

Indoor Distribution and ONT

Indoor riser and plenum routes favor LSZH jackets to meet smoke/flame codes. Flat drop cable forms strip cleanly and present controlled stubs for fast ONT terminations.

We guide the choice of steel or FRP (dielectric) strength members based on bonding needs, lightning exposure, and hardware compatibility. Standardized line prep shortens install time and reduces scrap.

Deployment Key feature Field note
Overhead Self-supporting, steel or FRP Verify messenger hardware/tension
Duct Low-friction, crush-resistant Use pull tape and proper lubricant
Direct burial PE jacket, moisture barrier Follow depth/warning tape codes
Interior LSZH with tight-bend support Maintain bend radius at penetrations

Our approach delivers a consistent installation across indoor/outdoor transitions. That leads to fewer callbacks, speeds activations, and reliable field performance for your system.

End-to-end support and after-sales service

Our team coordinates testing, scheduling, and installation guidance to remove surprises during deployment.

Shanghai Weiye OFC Equipment offers engineering support from early requirements through approved drawings and pilot builds. We provide doc templates and clear installation notes so field crews share a unified plan.

After-sales service covers rapid response, root-cause analysis, and corrective actions. All products ship with full test reports and traceability to support QA acceptance.

  • 24/7 availability for status and technical support.
  • Warranty with free replacement if any quality problems are confirmed.
  • Coordination of line schedules for urgent changes or acceleration requests.
  • Config control so shipped items match agreed specs consistently.
Support area What we do Benefit
Engineering Spec review & pre-production builds Reduced field issues
QA/Testing Lab trials & 100% test reports Traceable quality
Service Rapid replacement & root-cause Minimized downtime

Wrap-Up

Select Shanghai Weiye OFC Equipment for custom drops, quick lead times, and full traceability.

We deliver customized FTTH drop solutions that combine materials with validated manufacturing and lab tests. Every reel includes a 100% test report and documented lab trials to support U.S. field acceptance.

A robust production line, including CLX-BPO2 prep assets, reduces variability and speeds turnaround. Our equipment set standardize strip/stub lengths so installers see consistent results at turn-up.

From fiber selection through jacket, printing, and packaging, we balance performance and cost to extend service life. Dedicated support guides scheduling, logistics, and after-sales care so your deployment stays on plan.

Contact Shanghai Weiye OFC Equipment to align specs, timeline, and volume. We stand behind every shipment with lab validation and responsive service.

Related: Comparing Compact Fiber Units: Features and Performance

Key Metrics to Evaluate a Plastic Mold Company

China Injection Molding Sourcing: A Complete Guide

Well, the major meeting has just concluded. your new product is a go, the timeline is aggressive, and the budget is, let’s say, constrained.. Then a voice—perhaps your manager or the CFO—drops the line that gives every project manager a shock: “We should look at sourcing this from China.”

You nod, of course. It seems sensible at first glance. The potential savings can be massive. However, your brain is racing with concerns. You know the rumors, don’t you? Quality failures, endless communication gaps, shipments arriving months late and nothing like the prototype. It feels like walking a thin line between big savings and total project failure.

Here’s the thing, though. Sourcing China injection molding can be a calculated project. It’s no different from any structured project. And as with any project, success depends on your methodology. It isn’t about the cheapest offer but about choosing the right supplier and running the process transparently. Ignore the nightmare anecdotes. Let’s go through a step-by-step guide to succeed.

China injection molding

Step One: Do Your Homework

Before you even whisper the word “supplier” or open a browser tab to Alibaba, you need to get your own house in order. In fact, most overseas manufacturing headaches stem from a vague or incomplete RFQ. You cannot expect overseas partners to interpret your unspoken requirements. A vague RFQ is like telling a contractor to bid on “a house.” You’ll get wildly varied quotes that are useless.

Your RFQ should be bulletproof—clear, detailed, and unambiguous. It’s the cornerstone of your entire effort.

What should you include?

First, your 3D CAD files. These are non-negotiable. Provide files in common formats (e.g., STEP, IGS) to prevent import issues. This is the master blueprint for your part’s geometry.

But 3D isn’t enough. Add comprehensive 2D plans. This details critical info missing from the 3D file. I’m talking about critical tolerances (like ‘25.00±0.05 mm’), material specifications, required surface finishes, and notes on which features are absolutely critical to function. Call out smooth surfaces or precision hole sizes in big, bold notation.

Then specify the material. Don’t just say “Plastic.” Don’t even just say “ABS.” Be specific. Specify SABIC Cycolac MG38 in black, if that’s the resin you need. Why be exact? Because there are thousands of plastic variations. Naming the precise grade locks in the mechanical, thermal, and aesthetic properties you need with plastic mold injection.

A good supplier can suggest alternatives, but you need to give them a clear starting point.

Finally, include the business details. What is your Estimated Annual Usage (EAU)? They need clarity: is it 1,000 total shots or a million units per annum? Tool style, cavity count, and unit cost are volume-driven.

Finding the Right Supplier

With your RFQ perfected, now, who do you send it to? The internet has made the world smaller, but it’s also made it a lot noisier. It’s easy to find a supplier; it’s hard to find a good one.

You’ll probably kick off on Alibaba or Made-in-China. They offer breadth but not depth. Use them to build a shortlist, not the final list. Aim for a preliminary list of 10–15 potential partners.

Still, you must dig deeper. Consider using a sourcing agent. True, they charge a fee. Yet top agents deliver reliable, audited suppliers. They bridge language and cultural gaps. For a first-time project, this can be an invaluable safety net. Consider it timeline insurance.

Another classic method? Trade shows. If you can attend, shows such as Chinaplas transform sourcing. Meeting onsite is unbeatable. Inspect prototypes, interview engineers, and sense their capabilities. Plus, ask peers for referrals. Ask other project managers in your network. A recommendation from a trusted peer is often worth its weight in gold.

Sorting the Contenders from the Pretenders

With your RFQ dispatched to dozens of firms, bids begin to arrive. Some prices will undercut logic, others will shock you. Now, sift through and shortlist 2–3 reliable candidates.

How to proceed? It involves both metrics and gut feel.

First, look at their communication. Is their turnaround swift and concise? Do they communicate effectively in English? But the key: do they probe your RFQ? Top vendors will critique and inquire. Example: “Should we add draft here for better ejection?” or “Your tolerance may require extended CMM time—okay?” That’s a huge positive sign. It shows they’re engaged and experienced. A “Sure, no issues” vendor often means trouble.

Next, dig into their technical capabilities. Get their tooling inventory. More importantly, ask for case studies of parts they’ve made that are similar to yours in size, complexity, or material. A small-gear shop won’t cut it for a big housing.

Finally, inspect the factory. This is not optional. As you vet staff, you must vet suppliers. You can travel or outsource a local inspector. They perform a one-day factory inspection. They will verify the company is real, check their quality certifications like ISO 9001, assess the condition of their machinery, and get a general feel for the operation. It’s the best few hundred dollars you will ever spend on your project.

Transforming CAD into Real Parts

Once you’ve chosen your supplier. you agree on 50% deposit to start toolmaking and 50% balance after sample sign-off. Now the real fun begins.

Your supplier’s first deliverable is a DFM analysis. Design for Manufacturability (DFM) is essential. It’s their professional review of your CAD. The report calls out sink-risk zones, stress-causing corners, and draft angle gaps. A detailed DFM shows expertise. It becomes a joint effort. Together, you tweak the design for best manufacturability.

Once the DFM is approved, they’ll start cutting steel to make your injection mold tool. A few weeks later, you’ll get an email that will make your heart beat a little faster: “T1 samples have shipped.” These represent the first trial parts. It’s your first real test.

T1 parts usually require adjustments. It’s par for the course. There will be tiny imperfections, a dimension that’s slightly out of spec, or a blemish on the surface. You’ll provide detailed feedback, they’ll make small adjustments (or “tweaks”) to the tool, and then they’ll send you T2 plastic mold samples. It could require several iterations. Plan for this loop in your schedule.

At last, you get the perfect shot. Dimensions, finish, and performance all check out. This is your golden sample. You ratify it, and it becomes the quality yardstick for production.

Crossing the Finish Line

Getting that golden sample feels like the end, but it isn’t. Next up: mass manufacturing. How do you ensure that the 10,000th part is just as good as the golden sample?

You need a clear Quality Control plan. Often, you hire a pre-shipment inspection service. Again, you can hire a third-party service. For a few hundred dollars, they will go to the factory, randomly pull a statistically significant number of parts from your finished production run, and inspect them against your 2D drawing and the golden sample. They’ll send you a detailed report with photos and measurements. Only after you approve this report do you authorize the shipment and send the final payment. This audit shields you from mass defects.

Finally, think about logistics. Know your shipping terms. Are you on FOB terms, where they load and you take over? Or EXW, where you handle everything from their gate? These details have a big impact on your final landed cost.

Sourcing from China is a marathon, not a sprint. It’s about building a relationship with your supplier. Treat them like a partner, not just a line item on a spreadsheet. Open dialogue, trust, and rigorous procedure deliver results. It’s a challenging project, no doubt. But with this framework, it’s one you can absolutely nail, delivering the cost savings everyone wants without sacrificing your sanity—or the quality of your product. You’re set to succeed.

Precious Metal Recycling Companies: Defining Key Service Offerings

Your Guide to Green Precious Metal Recovery

Did you know that more than $60 billion worth of precious metals are discarded each year in electronic waste alone? This staggering figure underlines the critical role of precious metal recycling. Not only does it boost economic health, it also protects our environment. When we recover gold, silver, platinum, and palladium, we reduce pollution and conserve resources.

Leaders such as Dongsheng Metal Trading are paving the way for sustainable recycling. They guarantee that valuable metals return to use instead of filling dumps. Such a precious metals recycling model drives eco-friendly recycling and sustainable methods.

Key Highlights

  • Over $60 billion in precious metals is disposed of in electronic waste annually.
  • Recycling precious metals shrinks environmental harm and saves resources.
  • Key precious metals are gold, silver, platinum, and palladium.
  • Green recycling methods are essential for a sustainable future.
  • Recycling experts like Dongsheng Metal Trading lead the industry.

Exploring Precious Metals and Their Worth

Precious metals are rare, naturally occurring metallic elements that have captured the interest of investors and industries alike. Examples include gold, silver, platinum, and palladium, each prized for special traits. Notable traits are excellent conductivity, corrosion resistance, and rarity. Given the resource-intensive mining and processing, recycling precious metals is essential.

precious metal recycling

Market demand and each metal’s properties drive its value. Recycling precious metals plays a critical role in sustaining the supply chain. It also reduces environmental impacts associated with mining activities. By thorough recycling, these metals return to their pure form. This preserves finite resources while yielding economic benefits.

Precious Metals Explained

Precious metals possess unique characteristics that make them desirable for a variety of applications. Scarcity plus special properties drive their economic importance. Notable examples are:

  • Au: Prized for its shine and tarnish-proof nature.
  • Ag: Recognized for its versatility and high conductivity.
  • Pt: Celebrated for its durability and catalytic properties.
  • Palladium: Gaining traction in cars and electronics.

Reasons to Recycle Precious Metals

The practice of recycling precious metals has emerged as a vital component for sustainability. It helps conserve these finite resources and significantly reduces the ecological footprint tied to traditional mining. Consider these advantages:

  • Cutting down mining-related environmental harm.
  • Using far less energy than fresh extraction.
  • Supporting a circular economy via material reuse.
  • Economic upside from extracting high-value resources.

The Importance of Precious Metal Recycling

Recovering metals delivers big eco and financial wins. Pointing out these perks shows how to shrink our eco-impact. Plus, it spurs economic development and steadiness.

Environmental Benefits

Green gains from metal recycling are huge. When we recover metals from e-waste and scrap, landfill volume drops. This reduces the need for new mining, conserving natural resources.

It lessens mining impacts, including ecosystem harm and contaminants. A focus on metal recovery moves us toward real sustainability.

Financial Gains

Economic upsides of recycling stand out equally. Recycling precious metals can lower manufacturing costs. It lets businesses choose reclaimed over freshly mined metals.

This shift creates jobs in recycling facilities and boosts market stability as demand for recycled metals grows. By leveraging these economic advantages, businesses can improve their profitability. They also contribute to a greener economy.

The Precious Metal Recycling Process

Recovering precious metals involves multiple steps for peak efficiency. It starts with collecting metals from various sources like discarded electronics, jewelry, and industrial scraps. These materials then undergo sorting, cleaning, and analysis to determine their composition and value.

The Precious Metal Recycling Process

Such a methodical process ensures efficient recovery. Each step is designed to optimize the yield of precious metals. Sorting divides metals by kind and grade. Cleaning removes contaminants that could hinder recovery. Analysis identifies the concentration of precious metals, guiding the choice of recycling techniques.

Recycling Techniques Used

Advanced recycling techniques are employed to achieve high metal recovery rates. One method, thermal reduction, leverages heat to separate metals from base materials. Smelting and chemical baths extract and purify metals. Companies like Dongsheng Metal Trading use these methods to boost efficiency and maximize returns in the precious metal recycling process.

Which Precious Metals Are Recyclable

Scrap recovery benefits both Earth and economy. A host of precious metals are recyclable, aiding markets and ecosystems. It’s important for people and businesses to know which metals can be recycled.

Gold, Silver, and Platinum

Gold, silver, and platinum stand out among precious metals. You’ll see them in rings, currency, and industrial parts. Gold’s high price and use make it a prime recycling target. Silver recovery matters too, thanks to its role in imaging, tech, and solar.

Platinum, while rarer, finds value in catalytic converters.

Electronics Precious Metals

E-waste metals present special recovery opportunities. Devices such as phones and computers hold palladium and indium. Reclaiming them cuts e-waste and recovers key resources.

The need to recycle these metals is critical. Sectors strive to cut waste and boost recycling efficiency.

Who Gains from Metal Recycling?

Precious metal recycling is essential for several key industries, allowing them to use valuable resources efficiently and sustainably. Device manufacturing in electronics profits hugely from recovered metals. Aerospace and medical sectors also depend on these metals for critical components. Examining industry recovery uncovers eco- and economic advantages.

Electronics Industry

Electronics spearheads recovery, given the metal content in phones and PCs. Fast tech progress fuels growing e-waste volumes. This makes effective recycling of these metals, such as gold, silver, and palladium, critical. That saves resources and cuts mining carbon footprints.

Firms ramp up recycling to hit sustainability targets. Such a move upholds efforts to conserve and protect.

Aerospace and Medical Equipment

Metal recovery is key in aerospace and medical sectors where metals are in vital parts. Alloys prized for strength and anti-corrosion make up flight and medical components. Metal recovery slashes expenses and ensures eco-compliance.

These sectors know green recovery eases resource shortages. It also enhances operational efficiency, making recycling a key strategy for sustainability.

Selecting Recycling Partners

Finding trustworthy precious metal recycling companies is key to recycling effectively. Be sure to quiz them on their methods. Pricing models and processes make a big difference. By comparing services, you can see what each company offers and make a smart choice.

What to Ask a Recycler

  • Can you share your precious-metal recovery accreditations?
  • How do you process various precious metals?
  • Which recovery percentages do you achieve for each metal?
  • How do you handle pricing, and what additional fees might apply?
  • Do you have client testimonials or references?

Evaluating Offers

When searching for a recycler, it’s vital to compare different companies based on their services. Use a table to line up these factors:

Company Name Recovery Rate (%) Processing Fee ($) Turnaround Time (Days)
Recycling Co. A 95 50 7
Recycling Co. B 90 45 5
Recycling Co. C 92 55 10

Comparing options ensures you get top value and service. This ensures you get the most value and meet industry standards.

Precious Metal Recycling: Your Eco-Friendly Guide

Understanding how recyclers operate is key for those interested in precious metal recycling. They handle all stages, from gathering to final refining. This ensures maximum efficiency and value from metals.

Recycler Operations

Advanced workflows—assay, separation, smelting—unlock metal value. Collection comes from devices, jewelry, and industrial waste. Next, they employ precise methods to sort metals. Next, they refine these metals to extract precious elements like gold, silver, and platinum.

That workflow both boosts recovery and promotes green methods. It’s a critical step towards sustainable development.

Choosing the Right Recycler for Your Needs

You’ll want to weigh several factors in your choice. Begin by checking their green credentials. A focus on sustainability is non-negotiable. Next, review their service range—from pickup to refining.

Pricing is another key factor. Gather price quotes for side-by-side comparisons. Firms such as Dongsheng Metal Trading tailor services to each sector. They remain a trusted partner for targeted recovery.

Types of Recycling Facilities

Metal recycling is a critical sector for sustainable practices and waste management. There are specialized centers for different metals and materials. Awareness of facility types guides you to proper recyclers. That supports firms and ecosystems alike.

Recycling Center Types

There’s a broad spectrum of recycling operations. Some yards recover gold and silver; others accept all metal waste. Here are a few common types:

  • Scrap yards process a broad mix of metal types.
  • High-value metal recyclers provide precision recovery for gold, silver, platinum, etc.
  • E-waste hubs target valuable metals inside tech devices.

Facility Access Factors

Accessibility to recyclers is key for efficient metal recovery. Companies should evaluate haulage considerations. Key access factors include:

Factor Description
Proximity Closer sites cut shipping costs and delays.
Partnerships Connections with nearby facilities speed up recycling.
Service Range Knowing each facility’s offerings guides your choice.

Choosing appropriate centers and easy access drives recovery efficiency.

Electronic Waste Recycling and Precious Metals

Electronic waste is a pressing issue in today’s world, causing environmental harm. Discarded devices often contain precious metals that can be recovered through recycling. This highlights the importance of seeing e-waste as a valuable resource.

Metals in Devices

Many electronic devices hold small amounts of precious metals like gold, silver, and palladium. These metals are found in various parts:

  • Circuit boards
  • Connectors and ports
  • Capacitors and resistors
  • Battery terminals

Even everyday items like smartphones, laptops, and TVs are filled with these metals. By recycling, we retrieve and reuse these valuable elements.

The Importance of E-Waste Recycling

Recovering e-waste metals safeguards the environment and reclaims materials. It trims dump loads and conserves raw materials. The benefits of recycling e-waste metals are clear:

  • It cuts ecological hazards from poor e-waste handling
  • It cuts down on carbon emissions through eco-friendly practices
  • It bolsters circular models by returning scrap to production

Encouraging electronic recycling promotes sustainable resource management. It secures a healthier planet for tomorrow’s children.

What’s Next in Metal Recycling?

The field of precious metal recycling is undergoing a transformation, driven by technological progress and a surge in sustainability efforts. Facing resource limits, recyclers embrace new methods. They are embracing new methods and processes, setting the stage for the future of recycling precious metals.

Trends in Sustainable Recycling

Modern green recycling strives to cut waste and eco-damage. Companies are shifting towards eco-friendly practices, like using biodegradable packaging and energy-efficient processes. These changes align with global sustainability objectives, pushing industries towards more responsible and planet-friendly behaviors.

New Metal Recovery Tech

Breakthroughs in recovery boost metal recycling yields. Automated sorters and hydrometallurgy ramp up yield. They ramp up yields and shrink eco-footprints, advancing metal recycling.

Starting a Precious Metal Recycling Venture

Starting a precious metal recycling business demands meticulous planning and a deep grasp of operational and market dynamics. Founders need a roadmap, regulatory know-how, and solid groundwork. That means in-depth market analysis and client identification. Securing licenses and legal compliance is crucial for long-term viability.

Steps to Establishing a Business

Setting up a precious metal recycling venture requires several essential steps:

  1. Conduct market research to understand needs and rivals.
  2. Develop a detailed business plan outlining goals and strategies.
  3. Acquire suitable recycling equipment that meets your operational needs.
  4. Obtain capital via loans or investors.
  5. Secure regulatory approvals and certifications.
  6. Launch marketing to attract clientele.

Compliance and Certifications

Grasping legal frameworks is essential for your recycling venture. Meeting environmental rules protects your operation and the planet. Must-know compliance points:

  • Obtaining official certification from governing bodies.
  • Following all levels of waste and recycling regulations.
  • Training staff in safety protocols and best practices.

To Conclude

Precious metal recycling is essential for preserving natural resources and improving environmental health. It helps people and companies cut waste’s ecological toll. The recovered metals reduce mining needs and boost the economy by creating jobs in recycling.

Metal recovery delivers both eco and economic upsides. Working with Dongsheng Metal Trading guarantees green standards. This collaboration strengthens the circular economy, benefiting both recyclers and consumers.

Our path to sustainability relies on united metal recovery initiatives. Growing awareness can lead to a society that values responsible consumption and environmental care. Embracing these steps helps today and protects tomorrow’s world.

FTTH Cable Production Line Throughput Optimization

State-of-the-Art FTTH Optical Cable Assembly Line Gear Systems

Did you ever consider the impact of high-speed internet cable demand on FTTH cable production systems? With our need for fast, reliable connectivity intensifying, industry leaders like HONG KAI and Nextrom are revolutionizing production. They are rolling out cutting-edge cable equipment to boost production efficiency. Not only does this shift slash operational costs but also enhances high-speed internet cable quality, satisfying today’s market standards.

Here, we’ll examine the pioneering equipment and methods reshaping SZ stranding line manufacturing. Discover how these advancements are set to revolutionize the fiber optic sector.

Summary Points

  • Understanding the importance of FTTH cable production line equipment in high-speed internet access.
  • Examining the significant role of companies like HONG KAI and Nextrom in driving technology innovation.
  • Discovering the benefits of adopting advanced cable equipment in manufacturing processes.
  • Recognizing how enhanced cable quality is critical for meeting consumer demands.
  • Acknowledging the importance of production efficiency in a competitive market.

Understanding FTTH Cable Production Line Technology

The creation of fiber optic cables, especially for FTTH technology, involves a complex blend of state-of-the-art tools and precise methods. Contemporary production of these cables includes various components that boost efficiency and quality. Knowing these elements sheds light on the progress toward next-level production systems.

Core Components of Modern Fiber Optic Cable Manufacturing

Today’s fiber optic cable making includes:

  • Extrusion systems for coating and insulating fibers
  • Fiber tension control mechanisms to maintain optimal fiber quality
  • Automated operations that simplify production processes

These elements work together to produce a dependable and durable product. For instance, state-of-the-art temperature control systems guarantee consistent conditions. Automated adjustments also reduce human error.

Evolution from Traditional to Advanced Production Systems

The shift from traditional to advanced systems marks a significant leap in technology and methods. Earlier, manual methods have been superseded by automated systems. This change has led to:

  1. Increased productivity and shorter production times
  2. Reduced waste due to precise material handling
  3. Improved product quality thanks to tighter quality control

Key Technologies Driving Industry Innovation

Several core technologies are propelling innovation in the fiber optic field. These include:

  • Precision temperature control that regulates and maintains optimal production conditions
  • Automatic settings that adapt to varying production requirements
  • Advanced monitoring systems providing real-time feedback on production quality

Thanks to these technologies, manufacturers can ensure their fiber optic products meet the high standards required for FTTH applications.

Essential Equipment for Fiber Secondary Coating Line Operations

In the world of fiber optic cable manufacturing, the fiber secondary coating line is key. It safeguards fiber optics through efficient coating processes. With technology evolving, having the latest equipment is critical for optimal production and reliability.

High-Speed Secondary Coating Processes

Advances in secondary coating processes have dramatically improved manufacturing efficiency. Contemporary systems can now handle increased volumes, addressing rising demand. These processes apply coatings that enhance durability and performance, resulting in superior fiber cable products.

Single and Dual Layer Coating Applications

It’s important to differentiate between single and dual layer coatings in the fiber secondary coating line. Single-layer coatings offer basic protection, while dual-layer coatings add extra resistance to environmental stressors. Both methods employ high-speed processes for even coating application, guaranteeing fiber optics perform longer in various conditions.

Temperature Control and Curing Systems

Temperature control systems are vital for curing coatings during production. They ensure the right conditions for adhesive substances in the fiber secondary coating line. Accurate temperature management allows for ideal curing times and conditions, resulting in higher quality fibers ready for real-world use.

Fiber Draw Tower and Optical Preform Processing

The fiber draw tower is crucial in optical preform processing and cable manufacturing. It draws the preform into thin fiber strands, guaranteeing superior fibers with exceptional clarity and strength. The tower’s environment is carefully controlled to achieve precise dimensions and physical properties.

Optical preforms serve as the foundation of this process, defining the fiber’s final characteristics. The preform’s quality affects light transmission and durability. Advances in preform manufacturing have improved fiber ribbon line manufacturing efficiency.

Through innovative engineering and technology, the fiber draw tower and preform processing continue to evolve, addressing the growing demand for high-performance fiber optic cables. Quality at the preform level translates to better fiber optics, enhancing telecommunications and networking services.

Advanced SZ Stranding Line Technology for Cable Assembly

The SZ stranding line technology marks a major milestone in cable assembly, particularly for fiber optic cables. It provides precise stranding, critical for producing top-tier cables that meet strict standards.

Precision Stranding Equipment Features

The core of the SZ stranding line is its precision stranding equipment, which enhances cable durability and reliability. Its notable attributes include:

  • Advanced control systems that fine-tune settings in real-time for peak performance.
  • High-speed operation that boosts production efficiency.
  • Modular design for customization based on production needs.

Automated Tension Control Systems

Automated tension control systems are critical for maintaining consistency in stranding. They:

  • Ensure uniform fiber tension and strength distribution along the cable.
  • Lower defect rates, cutting down on waste and production costs.
  • Allow seamless integration of diverse materials, enhancing flexibility and performance.

Integration with Fiber Cable Sheathing Line

The integration of the SZ stranding line with the fiber cable sheathing line elevates production efficiency. This synergy enables for:

  • Streamlined workflows by minimizing manual intervention.
  • Consistent quality throughout the manufacturing process.
  • Higher throughput, addressing the growing need for superior cables.

Fiber Coloring Machine and Identification Systems

The fiber coloring machine is vital in telecom fiber cable production. It ensures each cable is identifiable and complies with color coding standards. Modern technology enables quick and accurate color application, boosting manufacturing efficiency.

High-Speed Coloring Technology

State-of-the-art machines use high-speed technology for consistent and fast color application. This cuts production time without compromising quality. The machines’ precision ensures accurate color application, helping adherence to strict color coding standards, essential for smooth installation and maintenance.

Color Coding Standards for Telecom Fiber Cables

Color coding standards direct manufacturers and technicians in the telecom industry. They organize fibers for easy identification, minimizing installation and troubleshooting errors. Each color represents a specific function or fiber type, guaranteeing clarity in complex networks.

Following these standards, supported by fiber coloring machines, improves safety and efficiency—a pillar of telecom operations.

Quality Control in Fiber Identification

Quality control is critical in fiber identification systems to meet market standards. Routine inspections during production check color accuracy and coding adherence. Sophisticated traceability systems trace fibers, improving product reliability.

This systematic quality control approach produces superior telecom fiber cable performance, delighting both manufacturers and end users.

Specialized Solutions for Fibers in Metal Tube Production

The production of fibers in metal tubes is a specialized domain in modern cable solutions. This method enhances durability and environmental resistance of optical cables, making them ideal for harsh conditions. Expert techniques encase fibers in metal, protecting them from damage and extreme environments.

In outdoor settings, where cables face harsh elements, these solutions demonstrate their worth. Manufacturers have engineered advanced methods to fortify and boost cable reliability, meeting the growing demand for durable communication systems. Precision SZ stranding line engineering and high-quality materials are integral in this process.

Employing specialized manufacturing methods ensures cables remain intact and reliable across industries. Companies emphasize innovative designs and strong materials to create high-performance optical cables for diverse environments and applications.

Fiber Ribbon Line and Compact Fiber Unit Manufacturing

The manufacture of fiber ribbons and compact fiber units is critical for modern telecommunication networks. This section explores the latest equipment and designs for these essential components. Innovators aim to meet the rising demand for high-density cable solutions in data centers.

Advanced Fiber Ribbon Line Equipment

Cutting-edge fiber ribbon line equipment allows efficient production of high-quality optical fibers. It integrates the latest technology to produce compact fiber units with top performance, minimizing waste and boosting throughput to suit various needs.

Compact Fiber Unit Design and Production

Compact fiber units are designed for space efficiency without sacrificing performance. Innovative methods shape these units for straightforward installation in diverse settings. These units are key for data centers, addressing the need for dense cables that save space and accelerate data transfer.

High-Density Cable Solutions for Data Centers

High-density cable solutions are critical for modern data centers, enabling faster data transfer and greater bandwidth. These solutions often incorporate fiber ribbons, produced through advanced processes. As data usage surges, these cables support robust infrastructure to meet today’s digital demands.

Optimizing High-Speed Internet Cables Production

Efficient production of high-speed internet cables is fundamental for today’s networks. The quality of FTTH cabling systems drives reliable connections. State-of-the-art manufacturing aims to boost performance while maintaining high standards.

Cabling Systems for FTTH Applications

FTTH cabling systems include designs that enhance signal transmission and cable longevity. They employ premium materials and innovative engineering to deliver fast, dependable internet for users.

Quality Assurance in Fiber Pulling Process

The fiber pulling process is critical in cable production, requiring meticulous attention. Quality checks prevent damage and maintain signal integrity. Integrated monitoring systems guarantee cable reliability and facilitate seamless installation.

Meeting Industry Standards for Optical Fiber Drawing

Adhering to industry standards in optical fiber drawing is vital for manufacturers. It secures production safety and cable reliability. Improving techniques and materials helps comply with these standards, yielding superior cabling systems.

Final Thoughts

The evolution of FTTH cable production lines has revolutionized telecommunications, allowing manufacturers to produce high-quality, reliable cables for today’s internet demands. As technology progresses, adopting advanced manufacturing solutions is essential to improve production efficiency while upholding top standards.

With the rising need for strong infrastructure, companies must adopt innovative methods in their FTTH cable production. These modern approaches improve cable reliability and support sustainable manufacturing in the fiber optic sector.

To stay ahead in the fiber optic cable industry, embracing these advanced solutions is critical. The future of cable production hinges on such innovations, ensuring telecommunications infrastructure can meet the growing global internet demands.

Related: Training Workers For FTTH Cable Production Line Efficiency

Charger Manufacturers in China Quality vs Cost Analysis

Best EV Charging Cable Manufacturers for Your EV

EV adoption is booming, with the demand for trustworthy and high-performance charging solutions surging. Currently, industry leaders have been at the forefront of this change, providing premium charging infrastructure. Southwire, for instance, entered the market in 2014 and excels, boasting over 1000 five-star reviews and a 75-year legacy in electrical construction.

The surge in electric vehicle adoption drives demand for long-lasting, quick, and safe EV Charger Manufacturers. Top manufacturers are developing to address changing requirements, offering solutions that boost the overall charging experience.

Grasping the differences between various charging solutions matters for making informed decisions. Quality charging infrastructure directly influences vehicle performance and customer satisfaction.

Notable Observations

  • Key suppliers deliver top-tier cables enhancing lifespan and protection.
  • EV market expansion drives need for high-efficiency chargers.
  • Industry leaders develop cutting-edge products for EV drivers.
  • Quality charging cables directly impact charging efficiency and vehicle performance.
  • Buying premium chargers pays off over time.

EV Charger Manufacturers

The Growing Importance of Quality EV Charging Cables

As more drivers choose EVs, the importance of premium EV charging cables is immense. The performance, security, and dependability of electric vehicle charging systems hinge upon the quality of the charging cables used.

How EV Charging Tech Has Advanced

Charging tech for EVs has evolved rapidly, with a focus on speedy charge times and improved safety features. Today’s EV charging cables are designed to meet these evolving needs, incorporating superior materials and construction techniques to minimize power loss and maximize transfer rates.

Why Quality Matters in EV Charging Infrastructure

Quality charging cables directly impact the overall performance and safety of EV charging infrastructure. Robustness, such as weather resistance and flexibility in extreme temperatures, maintain performance in harsh conditions. Moreover, regulatory compliance and adherence to industry guidelines are essential in guaranteeing safe operation.

Key Features Benefits
High-grade build quality Reduced energy waste
Robust durability All-weather reliability
Regulatory compliance Rigorous safety requirements met
Serviceability Long-term value proposition, reduced waste

Aichie Tech Electronics’ premium cables undergo rigorous testing at The Cable Lab. By opting for serviceable Portable EV Charger, users can save hundreds over a decade by choosing repairs over replacements, lowering environmental impact.

Top EV Charging Cable Manufacturers in China

A surge of cable makers in China supports the EV boom. They play a key role in global EV infrastructure, offering premium charging cables designed for various charging needs.

Wottz – Pioneers in EV Cables Since 2014

Wottz has been a leading cable manufacturer since 2014. They offer a range of cables that meet the specific requirements of EV charging systems, from Mode 1, 2, 3, and fast-charging Mode 4 DC Charging.

Aichie Tech Electronics – 75 Years in Electrical Solutions

Aichie Tech Electronics leverages 75 years of electrical expertise in its EV cables. Their products are built for residential and commercial applications.

Other Notable Manufacturers in the Market

Beyond industry leaders like Wottz and Southwire, other manufacturers are making their mark by focusing on specific automotive applications or technological innovations in electric vehicle charging. These include Type 1 & 2 connector experts, as well as companies developing cables with enhanced flexibility and resistance to environmental factors.

Understanding Different Types of EV Charging Cables

As electric vehicles become increasingly popular, understanding the various types of EV Charging Cable Manufacturers is crucial for optimal charging experiences. Different cables suit different charging needs. The variety in EV charging infrastructure demands a closer look at the cable options.

Type 1 vs Type 2 Explained

Type1 and Type2 charging cables are two common standards used for EV charging. Type 1, also known as SAE J1772, is North American standard, while Type 2, or Mennekes, is the European norm. The choice between these cables depends on the vehicle’s connector type and the charging station’s compatibility. Type 2 cables often handle greater power, making them ideal for speed.

Level2 and DC Fast Charging Solutions

Level 2 AC cables charge faster, up to 19.2 kW. DC Fast Charging cables, on the other hand, provide rapid charging by converting AC power to DC within the charging station, delivering rapid fill-ups. These cables are key for highway charging, letting EVs charge in minutes.

Portable and Tethered Cable Options

Portable EV charging cables, such as “Granny chargers,” offer flexibility by allowing owners to charge their vehicles from standard household outlets. Tethered cables are attached permanently, providing a convenient but less flexible charging solution. The choice depends on the owner’s charging needs and preferences.

When selecting an EV charging cable, factors such as cable length, charging speed, and compatibility with the vehicle are crucial. For instance, portable charging cables range from simple L1 cords to full L2 kits. Vehicle-to-load (V2L) cables represent an emerging category, enabling EVs to power external devices.

  • Flexible granny chargers and L2 units suit various needs.
  • Fixed cables add convenience, removing cable management tasks.
  • Cable length is a critical consideration, with options ranging from 5-meter standard cables to 50-meter extended cables.

Key Features of High-Quality EV Charging Cables

High-quality EV charging cables are distinguished by several key features that ensure reliable and safe charging. These features are vital to safe, efficient charging.

Durability and Weather Resistance

Durability and weather resistance are paramount in EV charging cables. Manufacturers like Wottz and Southwire use RoHS-compliant recyclable compounds, ensuring they perform in harsh climates. Their serviceable design facilitates easy maintenance and promotes recycling.

User-Friendly Design

Cables need to flex yet remain tough. High-quality EV charging cables are designed to be flexible, making them easier to handle and maneuver. This flexibility is combined with rugged construction for lasting performance.

Regulatory Approvals

Approved safety marks ensure reliable performance. They ensure their products meet or exceed standards such as IEC62196 for connectors and UL2594 in North America. Rigorous third-party testing evaluates electrical safety, mechanical durability, and environmental resistance.

Certification Description Region
IEC62196 Connector safety standards International
UL2594 Standard for electric vehicle supply equipment North America
ROHS Restriction of hazardous substances International

By focusing on these key features, manufacturers can provide EV charging cables that not only meet the highest quality and safety standards but also enhance the overall user experience.

Cutting-Edge EV Cable Innovations

The latest developments in EV charging cable technology are revolutionizing the way we charge our vehicles, with a focus on speed, reliable data transfer, and eco-friendly materials.

Liquid Cooling for Rapid EV Charging

Liquid-cooled charging cables are emerging as a key technology for ultra-fast charging, enabling electric vehicles to charge at significantly higher speeds without overheating.

Advanced Connector Tech

Hyperboloid contact points improve electrical connection, ensuring stable communication and power flow.

Green Charging Cable Designs

Leading manufacturers are prioritizing sustainability in their cable designs, minimizing ecological footprint with RoHS-compliant, serviceable builds. For instance, companies like Aichie Tech Electronics and Wottz are adopting serviceable design philosophies and RoHS compliance to minimize waste and promote recycling.

Programs for cable recycling, non-toxic compounds, and TPU sheaths mark the eco shift.

Choosing the Perfect EV Cable

Choosing the right EV charging cable is crucial for efficient and safe charging. To make an informed decision, consider several key factors.

Connector Compatibility

Verify your car’s inlet and cable plug match. Your vehicle’s onboard charger capacity sets the upper limit for AC power.

Determining the Optimal Cable Length

Choose a cable length that suits your charging needs. A longer cable provides more flexibility but may be heavier and less manageable.

Considering Power Requirements and Charging Speed

Ensure cable amperage aligns with charger and car. Standard Level 2 home charging operates at 7.2 kW, but some vehicles support up to 19.2 kW with appropriate electrical service.

Mind these points to pick a cable that fits your EV lifestyle.

Why Choose Premium Charging Solutions

With EV growth unabated, premium cables are essential. Choosing cables from Wottz or Aichie Tech Electronics provides long-term value and reliability. Their serviceable designs enable repairs over replacements to cut waste. This approach supports eco-friendly EV use.

By choosing high-quality charging solutions, EV owners can enjoy peace of mind knowing their equipment is certified and compatible with future advancements.