THE ULTIMATE GUIDE TO AN SZ STRANDING LINE

Intermittent Bonded Ribbon Production Line Available For Sale

A specified speed of 600 m/min gives this equipment considerable production capacity for optical-fiber applications. Prospective buyers should confirm the achievable speed, machine setup, and required operating conditions directly with the manufacturer before proceeding.

Shanghai Weiye OFC provides a system engineered to manufacture 12- and 16-fiber rollable ribbons. Its product description presents the equipment’s capabilities, technical specifications, and included systems, providing U.S. buyers with a basis for comparing their equipment requirements.

Review the listed configuration in the product description, then contact the supplier about pricing, installation, and options specific to your project. This approach helps determine which equipment details apply to your particular manufacturing site and goals.

The listed address for Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. is 201 Minyi Road, Songjiang District, Shanghai. Consider the product listing a preliminary information source, and confirm up-to-date specifications and commercial terms with the supplier. Submitting a clear request for pricing and specifications can help you move forward with the assessment.


Important Points To Consider

  • A speed of 600 m/min is listed, but buyers should verify the operating conditions with the manufacturer.
  • This equipment supports production of 12-fiber and 16-fiber rollable ribbon formats.
  • Information about equipment functions, specifications, and included systems appears on the product page.
  • Request details about pricing, installation requirements, and project-specific customization.
  • A company address in Shanghai’s Songjiang District is included in the supplier information.

Overview Of The Intermittent Bonded Ribbon Production Line

According to the supplier, the equipment is designed for rollable IBR configurations containing 12 or 16 fibers. Its product page specifies a construction speed of 600 m/min and a fiber diameter of Ф245 μm ±10 μm. As these are manufacturer-listed values, confirm the actual production speed and relevant operating requirements directly with the supplier.
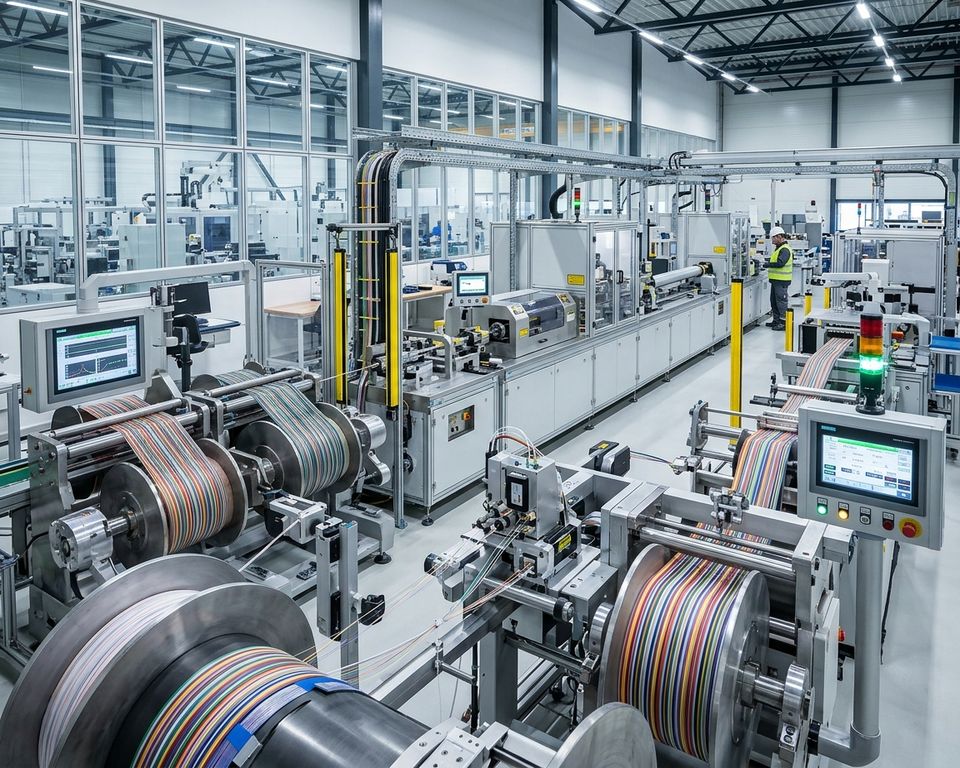
Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Designed To Produce Twelve- And Sixteen-Fiber Rollable Ribbons

Two fiber-count options are supported by the configuration for manufacturing rollable ribbons. This provides a useful reference when buyers compare machinery against their required ribbon format, fiber dimensions, and material-handling arrangements.

How Intermittent Adhesive Bonding Allows Flexible Fiber Configurations

The patent’s design examples describe neighboring fiber subunits joined by adhesive bonds positioned at intervals. One illustrated spacing range extends from 10 mm to 1,000 mm. This differs from a continuously bonded structure in which the connection extends across the full ribbon length.

By spacing the bonds apart, the assembly can move between a mostly planar arrangement and a rolled, curled, or folded shape. The specified spacing illustrates the patented design concept rather than confirmed production-machine settings.

  • Machine details: A choice of 12 or 16 fibers, a listed operating speed of 600 m/min, and a specified diameter of Ф245 μm ±10 μm.
  • Patent example: Adhesive-bond intervals ranging from 10 mm to 1,000 mm.
  • Design benefit: Flexible handling across several possible shapes.

Uses In Optical Fiber Cable Manufacturing

Flexible ribbon arrangements can help cable designers balance access for splicing with compact cable packaging. The patented design keeps fibers arranged in order while permitting sections between bonded points to shift as the cable is assembled.

Compact Cable Designs And High Fiber Density

For mass fusion splicing, an optical fiber ribbon can be arranged flat before being folded or rolled into a more compact cable. Potential advantages described in the patent include smaller cable constructions and an increased ratio of fiber area to overall cable cross-sectional area. The results achieved in practice depend on the complete cable construction and its intended use.

Ribbon Organization For Efficient Fusion Splicing

The ribbon format enables organized handling at the splice location while allowing the subunits to move during cable assembly. For production material planning, the listed specifications include payoff reels accommodating 25.2 km and 50.4 km of fiber. Buyers can evaluate these capacities against their production requirements and existing handling arrangements.

Design characteristic Possible application Consideration for buyers
Flat fiber configuration Mass fusion splicing Verify the needs of your splicing process
Folded or rolled format Compact cable packaging Examine the complete cable design
Payoff reels with capacities of 25.2 km and 50.4 km Planning material-handling operations Match the reel capacity to production operations

Specifications And Performance Of The Production Line

Before asking for pricing, assess whether the stated machine performance matches the demands of your production process. Reel compatibility and facility utility requirements are also important considerations for installation planning.

Production Speed, Fiber Diameter, And Attenuation

According to the specifications, the construction speed reaches 600 m/min. The specified fiber diameter is Ф245 μm ±10 μm, while additional attenuation is stated as ≤0.01 dB/km at 1550 nm. Ask the supplier to verify the testing conditions and achievable results.

Compatibility With Payoff And Take-Up Reels

The payoff system accommodates two reel dimensions, and the maximum weight of a full reel is 10 kg. The take-up assembly supports a T-type reel as well as a fiber-optic reel. Verify that your selected reel configuration is compatible with the facility’s material-handling process.

Site Utilities And Environment

The machine requires a three-phase, five-wire electrical supply rated at 380 V ±10%. The equipment should operate in an enclosed, clean, dry, draft-free area maintained at 15 to 25°C and a maximum relative humidity of 85%. Utility requirements also include nitrogen at 7 bar and 99.99% purity, plus a compressed-air supply at 6 bar. Verify the required utility connections before installation begins.

Specification Published requirement Installation planning note
Payoff reels Ф236 × Ф25.4 × 108 mm; Ф267 × Ф25.4 × 180 mm; maximum full-reel weight ≤10 kg Check reel compatibility and maximum weight
Reel used for take-up T-type reel: Φ410 × Φ50.8 × 391 mm, alternatively a fiber-optic reel Confirm compatibility with your selected format
Electrical and environmental requirements Power supply of 380 V ±10%; temperature of 15 to 25°C; humidity ≤85% Provide a clean, dry area without drafts
Gas supply Nitrogen at 7 bar and 99.99% purity; compressed air at 6 bar Check available gas capacity before equipment setup

Equipment For Fiber Payoff And Gathering

The payoff and gathering assemblies direct optical fibers into the ribbon-forming area. The associated controls help maintain a steady supply of fiber while reducing handling risks.

Tension-Controlled Payoff System For Sixteen Spools

The payoff assembly holds 16 spools and provides traversing along with separately adjustable tension settings. Each spool has a maximum weight capacity of 10 kg. Detailed specifications indicate a tension range of 0.4 to 2 N, accuracy of ±0.02 N, and a 550 W motor. Another overview gives a range of 40 to 150 g and accuracy of ±2 g, so buyers should confirm which specification applies to their configuration.

Fiber Guidance, Break Detection, And Static Control

The forming area receives fibers through U-groove guides, multi-groove gathering rollers, and devices designed to prevent jumping. Operators receive alerts about fiber problems through break detection and alarm functions. Safe handling is supported by protective guards and a pneumatic clamping mechanism. A rod-type electrostatic dust collector is positioned at the fiber exit, and additional anti-static devices help control dust throughout the gathering path.

Component Listed detail Intended function
Payoff 16 spools with a maximum of 10 kg each Supplies fibers using traversing
Motor and tension system Tension of 0.4 to 2 N, accuracy ±0.02 N; motor rated 550 W Supports regulated payoff of fibers
Guidance and safety Grooved rollers, alarms, guards, and pneumatic clamping Directs fibers and supports safe handling
Electrostatic management Rod-type dust collector and anti-static equipment Supports dust control along the fiber path

Precision Molding And Intermittent Adhesive Dispensing

Operators can adjust adhesive positioning and mold alignment through the forming platform. These settings allow the production process to be adapted to the intended ribbon configuration.

Adjustable IBR Mold Platform For Ribbon Formation

Ribbon formation uses three mold assemblies, each capable of holding up to five Nordson EFD jet valves. The mold adjustment range extends from 0 to 15 mm, while the mold base can be maintained between 20°C and 60°C. Precision valve groups mounted on sliding tables allow fine positioning and accurate application of adhesive dots.

Configurable Nozzle Arrangements For Twelve- And Sixteen-Fiber Ribbons

The 12-fiber configuration employs a 5+5+1 valve arrangement. The 16-fiber format is produced using a 5+5+5 valve layout. The control interface enables changes to dot count and spacing according to the ribbon configuration being manufactured. The process calls for a specialized adhesive suitable for both coating and curing.

Process setting 12-Fiber Format 16-Fiber Format
Dispensing valve layout 5+5+1 valve configuration 5+5+5 valve configuration
Mold positioning range 0 to 15 mm adjustment Adjustment range of 0 to 15 mm
Temperature of the mold base Temperature range of 20°C to 60°C 20°C to 60°C operating range

Curing Bonded Fiber Ribbons With UV-LED Technology

Adhesive across the fiber assembly is cured through a sequence of UV exposure stages. The arrangement of the ovens and their published operating values provide buyers with information for evaluating process compatibility.

Pre-Curing And Main Curing Stages

Pre-curing is handled by three specialized 800 W LED-UV ovens. Each oven processes fibers supplied by a separate mold group before the material reaches the main 6 kW post-curing oven. The system uses adjustable shutters to help contain UV exposure and minimize nitrogen losses. The supplier states a principal wavelength of 395 nm ±3 nm, minimum curing degree of 85%, and post-curing power of no less than 2.5 kW.

Nitrogen Management And Curing Performance

Operators can manually regulate nitrogen pressure and flow. Automatic functions also start nitrogen delivery during startup and stop it at shutdown. The manufacturer states that lamp-array power use remains at or below 80% of total power during steady, continuous operation at production speed. These specifications provide a reference for comparing equipment, although testing conditions should be verified with the supplier. Ask whether different adhesives or materials require adjustments to the settings.

Visual Monitoring, Capstan, And Take-Up

As fibers travel through the equipment, visual monitoring and steady winding support the maintenance of material quality. The published operating settings also offer buyers useful criteria for comparing equipment against their cable production requirements.

Real-Time Inspection Of Fiber Colors And Adhesive Dot Placement

A microscope and camera provide enlarged images in real time. Operators can inspect optical-fiber color order and verify the presence of resin dots at individual dispensing locations. This inspection helps identify ribbon problems before the material enters the winding stage.

Servo-Driven Traction And Precision Take-Up

A 1 kW AC servo motor powers the capstan’s Φ190 mm traction wheel. Metering accuracy is specified as better than 1‰. Operators can set tension between 50 and 500 g while maintaining an accuracy of ±5 g. These operating parameters help maintain careful fiber-ribbon handling as the material advances through the line.

Take-up operation is rated at 600 m/min with a spool weight limit of 30 kg. Servo-controlled winding and traversing systems help maintain consistent material placement. Cable pitch can be adjusted continuously between 1 and 6 mm. Position detection and direction changes are supported by a photoelectric sensor. Confirm that the operating conditions and settings are suitable for your target cable design with the supplier.

Production Monitoring And Electrical Control Systems

Accessible controls allow operators to adjust settings, check equipment status, and arrange orderly shutdowns. According to the manufacturer, the machinery incorporates Siemens controls alongside Schneider Electric switchgear.

Operating The Production Line Through PLC And Touchscreen Controls

Siemens S7-1200 and S7-1500 PLCs manage the ribbon manufacturing system through a 10.4-inch Siemens touchscreen. Low-voltage switchgear is supplied by Schneider Electric. Operators may control the entire line with interlocked units or run individual sections independently.

Settings, Alarms, And Length-Based Stops

Through the touchscreen, operators can manage process settings, activate curing ovens, configure wire feeding, and view alarms. Additional displays provide lamp runtime, real-time current readings, curing-oven temperature, and total machine operating hours. The meter-counter calibration feature allows displayed counts to be aligned with the distance actually traveled.

Operators can program a target production length that triggers deceleration or shutdown. This provides a practical way to control the end of a cable production run. Ask the manufacturer to confirm control capabilities and setup requirements before placing an order.

Control feature Listed detail Use
PLC controls and operator display Siemens S7-1200/S7-1500; 10.4-inch touchscreen Adjust and review operating information
Electrical control components Schneider Electric low-voltage switchgear Provides support for system control
Equipment monitoring and shutdown control Lamp, oven, runtime, and meter information with preset length Monitor production and stop or decelerate the equipment

Ribbon Quality, Material Selection, And Process Compatibility

The selected adhesive influences coating uniformity and the quality of the finished ribbon. The manufacturer calls for a specialized adhesive intended for the machine’s coating and curing process instead of an ordinary multipurpose product.

Dedicated Adhesive For Bonding And Curing

The pressure-fed adhesive system provides independent valve switches so each supply path can be opened or closed as required. Precision pressure-regulating valves help maintain controlled adhesive delivery at each dispensing location. Air pressure can be regulated but must remain at or above the listed minimum of 0.5 MPa.

The adhesive lines are black to reduce the risk of UV-triggered reactions while the system operates and cures material. Preventing unintended exposure matters because adhesive behavior could be affected before the material reaches the fiber surface.

Confirm suitable adhesives, process parameters, and surface-finish requirements with the manufacturer before choosing materials for a secondary coating operation. Discuss the material’s expected performance across your planned application and run duration. Detailed manufacturing guidance can support consistent quality throughout setup and the completed run.

Installation Requirements And Included Documentation

Ensure the workspace and utility supplies are ready before scheduling the machine’s installation. The supplier’s specifications provide guidance for planning the production site and supporting consistent operation of the fiber-optic machinery.

Required Facility Conditions And Connections Provided By The Buyer

The machine should be positioned inside a draft-free, enclosed workspace that is clean and dry. Keep the operating area between 15 and 25°C, with humidity at or below 85%. Provide nitrogen at 7 bar and 99.99% purity, along with compressed air at 6 bar.

The equipment package does not include connecting cables or cable trays. The buyer must arrange the principal power feed-in cable. Before installation, check cable routing and utility capacity, particularly when the machine will be located near secondary coating operations.

Documentation For Operation, Installation, And Maintenance

The supplier includes documentation supporting machine installation, operation, and servicing. Review these records before startup to help staff plan work activities and identify necessary supplies.

  • Instruction manuals, operating guides, and a general layout drawing
  • Electrical schematics, wiring diagrams, and drawings for installation and maintenance
  • Purchased-component instructions and a wear-parts list to support service preparation

The supplied records support preparation for commissioning and routine servicing of the cable production machinery.

Choosing A Ribbon Production Line For Your Manufacturing Needs

Begin by identifying the ribbon formats you intend to manufacture and sell. The machinery supports 12F and 16F formats and has a stated construction speed of 600 m/min. Assess the stated capabilities against your planned range of products, throughput requirements, and projected cable orders.

Verify take-up reel compatibility before placing an equipment order. The standard IBR reel has dimensions of Φ410 × Φ50.8 × 390 × Φ310 mm, supports up to 30 kg, and provides cable pitch adjustment from 1 to 6 mm. Check that these specifications suit your production facility and material-handling operations.

Payoff reel compatibility also deserves attention. Available options include international-standard spools accommodating 25.2 km, 50.4 km, and 63 km. Obtain the exact spool dimensions before ordering materials or planning the length of manufacturing runs.

In addition to speed, consider power and gas utilities, suitable adhesives, and the available monitoring functions. For cable manufacturing, determine whether the configuration suits fiber cable, loose tube, or another planned application. Before ordering, review equipment configuration and startup requirements directly with Shanghai Weiye. Checking equipment suitability in advance can reduce the likelihood of costly changes after purchase.

Planning point Manufacturer-listed specification Required buyer verification
Formats and speed 12F and 16F formats; 600 m/min Compare with target production and product mix
Take-up configuration 30 kg maximum capacity; adjustable pitch from 1 to 6 mm Verify that the reel and site arrangements are suitable
Payoff spools 25.2 km, 50.4 km, and 63 km spool capacities Verify exact spool dimensions

Request A Quote For The Intermittent Bonded Ribbon Production Line

U.S. buyers can evaluate a system offering 12F and 16F formats, a specified construction rate of 600 m/min, and specialized optical fiber ribbon-forming equipment. Compare these features with your planned cable products to assess equipment suitability.

When requesting a quotation, provide the required ribbon format, expected output volume, preferred reels, and available site utilities. Also describe the fiber type and handling requirements so Shanghai Weiye can evaluate the proposed configuration.

Before ordering, verify adhesive compatibility, the specified LED wavelength of 395 nm ±3 nm, and the published curing performance. Discuss how the stated specifications affect your intended material and finished surface-quality objectives.

Consult the product page for the published equipment description. Contact Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. to confirm machine configuration, delivery arrangements, and commissioning requirements. The company’s listed address is 201 Minyi Road, Songjiang District, Shanghai. You can call 021-60701630 to review your project needs with the supplier. Providing complete information in your quote request makes the following stages easier to clarify.
COMPARING FIBER RIBBON CABLE DESIGNS FOR DIFFERENT NETWORK ENVIRONMENTS

Intermittent bonded ribbon production line explained

Equipment for producing rollable formats in optical-fiber manufacturing is supplied by Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. Buyers can compare the capacity of this setup against their intended product range because it is designed for 12- and 16-fiber ribbons. Its split-type construction may also affect factory space and installation requirements.


For this specific production line, the listed construction speed is 600 m/min. The process combines fiber pay-off, gathering and guiding, intermittent resin dispensing, UV-LED curing, visual monitoring, capstan pulling, and take-up. The full process is important to evaluate, not just the stated speed.

Factory utilities, reel requirements, available floor space, and installation conditions should be assessed before purchase. Ask the supplier for its documentation package and check the system’s suitability for your cable design and operating requirements. Addressing these details in advance may reduce setup delays and support a smoother start.

Main Takeaways

  • Designed for rollable 12- and 16-fiber formats.
  • Specified equipment speed: 600 m/min.
  • Uses a split-type construction.
  • Curing, monitoring, pulling, and take-up stages are included.
  • Before purchasing, verify utilities, reels, installation requirements, and supplier documentation.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Explore The Intermittent Bonded Ribbon Production Line

To create rollable IBR formats, three mold groups position fibers for the application of small adhesive dots. Operators can adjust the mold position from 0 to 15 mm to support consistent spacing and shape.

Produce Rollable Fiber Ribbons With Precision Bonding

The machine is supplied by a 16-spool pay-off, and guide rollers with U-shaped grooves help maintain the organization of each strand. Steady contact during processing is supported by the rollers’ hard-anodized surfaces. For 12F and 16F layouts, the adjustable valve setup uses 5+5+1 valves for 12 fibers or 5+5+5 for 16. Ask the supplier to confirm tension control settings that suit your particular cable design.

Run 12- And 16-Fiber Configurations At Up To 600 m/min

The stated construction speed is up to 600 m/min. Pay-off reel options hold 25.2 km or 50.4 km of fiber according to the listed reel dimensions: Φ236 mm × Φ25.4 mm × 108 mm and Φ267 mm × Φ25.4 mm × 180 mm. The system also provides T-type or fiber-optic take-up reels. Compare reel capacity with your operational requirements and expected changeover time.

Examine The Production Line’s Main Equipment And Controls

Tension, resin placement, and UV exposure must work together to maintain reliable output. The system helps operators adjust settings to their cable design and fiber ribbon requirements.

Coordinate Fiber Tension, Resin Dispensing, And UV-LED Curing

Every pay-off unit uses electro-pneumatic adjustment. Dispensers can operate independently or in linked groups, with adhesive-dot spacing and counts configured through the interface.

Three pre-curing ovens serve the mold groups ahead of UV-LED post-curing. Ask the supplier to confirm resin compatibility and the relevant operating conditions.

The Siemens PLC and touchscreen display lamp current and oven temperature, generate alarms, and support preset lengths. Before purchase, review cabinet requirements and power supply needs.

Process Stage Technical Specification Buyer verification
Tension of fibers Pay-off: 0.4 to 2 N, ±0.02 N; capstan: 50 to 500 g, ±5 g accuracy Match settings to cable needs
Resin dispensing Independent or linked units; set adhesive-dot spacing and count Review interface settings
Curing With UV-LED Three 800 W pre-curing ovens; one 6 kW post-curing oven; 395 nm ± 3 nm; at least 85% cure under stable, high-speed conditions Verify compatibility with the resin
Monitoring Siemens S7-1200 or S7-1500 PLC; 10.4-inch touchscreen; live lamp current and oven temperature, alarms, preset lengths Check cabinet and power supply

Plan Installation, Operating Conditions, And Line Configuration

Before the machine is delivered, prepare a dedicated operating area. An enclosed, clean, dry, draft-free space is needed for the optical fibre system. Keep the temperature from 15°C to 25°C, with humidity at or below 85%. These conditions help safeguard fiber equipment and maintain precision during operation.

Review site utilities, electrical capacity, cabinet space, and cable design with your facilities team. Nitrogen at 7 bar with 99.99% purity and compressed air at 6 bar are required for the system. The electrical supply must be three-phase, five-wire, and 380 V ±10%.

  • Reserve room for the cabinet, components, resin, and access to service parts. Before starting the line, confirm the temperature settings and tension control.
  • Account for the specified reel size of Φ410 mm × Φ50.8 mm × 391 mm. The take-up unit accepts reels weighing up to 30 kg.
  • Account for the main power feed-in cable when preparing the site. The equipment package excludes connection cables and cable trays.

The supply scope, reel types, and installation needs should be confirmed before placing an order. Reviewing these items may reduce setup time and avoid subsequent delays. Ask the supplier to verify settings for your fiber and cable design, including lamp accuracy and operating conditions. Clear planning enables a smoother startup for the production system.

Request Pricing For A Ribbon Production Solution Tailored To Your Needs

Manufacturers seeking rollable 12- or 16-fiber formats can assess this line at its stated speed of 600 m/min. Share details of your fiber layout, output targets, cable requirements, reel preferences, and factory conditions to request a quotation.

Check the proposed system for its 16-spool pay-off, UV-LED curing setup, take-up capacity, and included options. Examine the supplied components, dispensing-head options, unit functions, and cable design prior to ordering.

Listed documents include operating and maintenance manuals, a general layout drawing, electrical schematics, and a wear-parts list. Reviewing these documents can help explain setup time and future service requirements.

Contact Shanghai Weiye Optic Fiber Communication Equipment Co., Ltd. to request pricing and configuration details that suit your output plan and site utilities. Verify the supply scope and replacement parts before purchase.

HIGH-PRESSURE EXTRUSION TECHNIQUES FOR FIBERS IN STAINLESS STEEL TUBE

A production line for intermittently bonded ribbon is instrumental in crafting flexible fiber groups for contemporary, high-count cable architectures. It maintains organized fiber alignment for expedited mass fusion splicing, yet accommodates the group’s flexibility within a compact cable core.

In contrast with fully bonded ribbons, intermittent bonded ribbons feature small bond points at predetermined intervals. This strategic placement allows fibers to remain aligned while the ribbon can conform to circular loose tubes and other confined spaces.

Fiber network engineers apply this technique when faced with constraints in duct space, splice closures, and equipment racks. A properly engineered ribbon cable facilitates dense network deployments in data centers, telecom backbones, metro networks, FTTx feeder systems, and 5G transport networks.


Key Takeaways

  • An intermittent bonded ribbon production line supports flexible, high-density fiber layouts.
  • Discrete bond points keep optical fibers organized without making the ribbon stiff.
  • Flexible ribbons help cable makers fit more fibers into compact circular cable designs.
  • Mass fusion splicing is faster when fiber order remains stable and clear.
  • Ribbon cable systems support data centers, telecom backbones, and fiber access networks.

Intermittent Bonded Ribbon Production Line Overview

This ribbon production method enables the creation of fiber designs that balance compactness with usability. This method involves applying bond points at controlled intervals, allowing for the movement of fiber subunits between these points.

This technique facilitates the incorporation of a higher number of fibers within constrained duct spaces. It also ensures the preservation of the organized ribbon structure, essential for efficient splicing and cable assembly processes.

How Does An Intermittently Bonded Optical Fiber Ribbon Work?

An intermittently bonded optical fiber ribbon connects adjacent fibers at specific intervals along its length. The segments between these bonds are left flexible, enabling the ribbon to adopt various configurations without rigidification.

This configuration is often referred to as a rollable, flexible, or spider web ribbon. It contrasts with the conventional flat ribbon cable, which maintains a fixed profile along its entire length.

For splice preparation, the fibers can be arranged into a flat ribbon for mass fusion operations. In cable production, the same fibers form compact bundles, optimizing space utilization within the cable.

Why High-Density Fiber Networks Need Flexible Ribbon Technology

Fiber network planners must address the challenge of increasing capacity within densely populated conduits, data centers, and access routes. The flexible nature of a flat cable structure allows ribbon groups to fit into smaller cable cores, preserving fiber order.

The fiber density ratio is a critical metric for network builders, comparing the space occupied by fibers to the total cable area. Intermittent bonding can improve this ratio, allowing ribbon groups to occupy available spaces within the cable.

For network installers, high-density fiber cables reduce the number of cables required for a given route. This design also supports high fiber counts without necessitating a rigid ribbon stack.

Intermittent Bonded Ribbon Production LineIntermittent Bonded Ribbon Production Line

Ribbon Feature Intermittently Bonded Ribbon Design Traditional Continuous Ribbon
Bonding pattern Discrete bonds at predetermined intervals Continuous bonding throughout the ribbon length
Fiber form between bonds Can roll, curl, or fold for compact packing Remains predominantly flat and planar
Splice preparation position Can be arranged flat for mass fusion splicing Is continuously maintained in a flat ribbon shape
Cable packing role Supports dense, flexible subunit placement Typically uses a fixed ribbon stack configuration
Typical cable application Compact high-density and flexible ribbon cable structures Traditional flat ribbon cable designs

Intermittently Bonded Ribbon Materials And Construction

A flexible bonded ribbon integrates precise fiber placement with adaptable bonding points. Its architecture enables high-density cable structures while allowing effortless separation during handling, routing, and splicing.

The selection of materials significantly influences ribbon width, peel characteristics, and durability. Each optical fiber subunit must maintain its fibers securely without imparting undue stiffness to the ribbon.

Optical Fiber Counts And Subunit Arrangement

Flexible bonded ribbons may support 4, 8, 12, 24, or up to 36 fibers. The choice of fiber count is determined by cable capacity, available duct space, and the requirements of subsequent mass fusion splicing.

A typical 12-fiber design may use six subunits, with two adjacent fibers in each subunit. The fibers within a subunit may be in contact or separated by no more than one and a half times the fiber diameter.

The inclusion of small gaps between subunits ensures ribbon flexibility. These gaps typically span from 5 to 100 micrometers, while the fibers remain aligned side by side across the ribbon width.

Ribbon Construction Element Common Arrangement Production Purpose
Ribbon fiber count 4, 8, 12, 24, or as many as 36 fibers Aligns fiber count with cable density and splice capacity
Fiber subunit layout Two neighboring fibers in each optical fiber subunit Supports controlled separation between groups
Fiber spacing in a subunit Touching or up to 1.5 fiber diameters Maintains a compact and stable profile
Gap between subunits 5 to 100 micrometers Improves flexibility at bond locations

Wet-On-Wet Bonding And UV-Curable Resin

Subunit coatings and bonding materials frequently employ UV-curable resin systems. Wet-on-wet bonding involves applying the bond material to the uncured subunit coating, which then cures together under UV energy.

This process creates a diffusion zone where the materials interact. For intermittent bonded ribbons, this zone can range from 2 to 50 micrometers, with 5 to 15 micrometers being the typical focused process range.

UV-curable resins can intermingle at the interface before curing. This supports molecular interaction between the bond and the optical fiber subunit coating, resulting in bonds that are both secure and flexible.

Essential Equipment In An Intermittent Bonded Ribbon Production Line

A fiber ribbon line integrates advanced motion control with meticulous material handling. Each station helps fibers stay clean, aligned, and stable from the initial payoff to the final winding.

The production equipment supports adjacent fiber placement, subunit coating, intermittent bonding, UV curing, cooling, inspection, and take-up. This sequential process enables manufacturers to manufacture customized flexible ribbon, preserving the integrity of the fiber order.

Fiber Payoff With Tension Control

Payoff units deliver individual optical fibers at a consistent rate from spools. Guides, rollers, and tension sensors prevent sudden pulls, averting twist, slack, or uneven spacing.

During ribbon production, maintaining balanced fiber paths before alignment is critical. Stable tension is essential for forming flat subunits and ensuring accurate color sequence control.

Discrete Bond Applicator And Coating Die

The coating system applies a UV-curable material around groups of two or more fibers. This material defines subunits while maintaining fibers in a flat, parallel layout.

A discrete bond applicator then places a second resin between neighboring subunits at planned intervals. This spacing allows the ribbon to flex and separate when needed, a critical aspect of custom ribbon cable design.

Equipment Core Function Manufacturing Benefit
Payoff tension system Supplies fibers under controlled tension Minimizes twisting and uneven fiber loading
Subunit coating die Forms coated fiber subunits Keeps subunit dimensions and shape consistent
Intermittent bond applicator Deposits resin at set intervals Provides controlled flexible bonds between subunits
UV cure and take-up system Handles UV curing, cooling, inspection, and final winding Helps protect bond quality and organized fiber placement

Ribbon Take-Up, Cooling, And UV Curing Equipment

UV lamps cure the subunit coating and intermittent bonds while the resin is wet. This wet-on-wet process forms a cohesive interface between materials, influencing bond strength.

The cooling stage lowers ribbon temperature before inspection and winding. The fiber ribbon line may also employ vision checks to monitor width, bond position, and surface quality.

Take-up equipment winds the finished ribbon with low, even tension. Proper winding protects the cured ribbon structure, ensuring the custom ribbon cable is ready for later cabling, splicing, or connector assembly.

Fiber Preparation, Alignment, And Color Sequence Control

The foundation of a stable ribbon cable with fiber preparation. Each strand must enter the assembly clean, centered, and in the correct sequence before the coating and bonding processes commence.

Fiber Identification Management For Splicing And Maintenance

Consistent fiber color identification is indispensable for splicing, testing, and maintenance operations. The standard 12-fiber sequence, typically consisting of blue, orange, green, brown, slate, white, red, black, yellow, violet, rose, and aqua, facilitates swift identification.

With higher fiber-count cables, the sequence may be repeated within controlled subunits. This method ensures that each ribbon cable remains organized within splice trays, closures, and cable connector layouts.

Fiber Number Fiber Identification Color Process Purpose
1 Standard blue Starts the standard fiber color sequence
02 Orange Allows quick identification during handling
03 Green Maintains the specified planar order
4 Brown Helps verify subunit placement
05 Slate Creates a clear mid-sequence identifier
6 White Improves visibility during inspection
7 Red Helps maintain accurate splice documentation
8 Standard black Supports sequence identification inside splice trays
09 Yellow Supports rapid identification during restoration work
10 Violet Helps distinguish later positions in the standard sequence
11 Rose Supports high-count ribbon identification
12 Standard aqua Completes the standard color order

Preventing Fiber Twisting And Uneven Tension

Payoff systems and guides are essential in maintaining fibers in a flat, side-by-side configuration. This prevents twist, crossing, and gaps that could alter the ribbon’s width or distort the bond pattern.

Operators meticulously monitor tension across every path before the fibers reach the coating die. Proper alignment is critical for mass fusion splicing and ensures the finished ribbon cable fits its intended cable connector system.

Intermittent Bond Application And UV Curing Process

The intermittent bonding process joins fiber subunits without solidifying the ribbon into a rigid form. This method facilitates compact routing and ensures dependable handling within a flexible flat cable. It also aids in maintaining the planned fiber layout during subsequent cable assembly.

Applying Bonds At Predetermined Intervals

The production equipment applies bonding points at intervals ranging from 10 mm to 1,000 mm. The bond locations may stagger along the ribbon’s length. This arrangement provides support to adjacent subunits while allowing sufficient free length for movement.

A precise applicator dispenses a measured amount of UV-curable resin at each bond point. Bonds often exhibit a diamond-like shape, with wider centers and narrower ends. The tapered ends help minimize localized stress changes when the cable bends or twists.

Creating Strong, Flexible Bond Interfaces

Wet-on-wet processing requires applying a second material before the first subunit coating cures. The uncured layers can blend before undergoing a shared UV curing step. This approach fosters a gradual interface, unlike a sharp material boundary.

The resulting material gradient affects various properties, including color, Young’s modulus, and surface friction. Bond ends may feature saddle-like surfaces with both convex and concave curves. These features help the bond resist peeling while facilitating separation when required.

Controlling UV Curing Performance

UV curing systems must deliver consistent energy across the ribbon. Factors such as line speed, lamp output, resin volume, and exposure time impact the bond’s quality. Selecting the right UV-curable resin ensures rapid curing without compromising the fiber coating.

Process personnel carefully track bond shape, cure level, and ribbon flexibility during production. The cured cable should transition smoothly from a flat plane to various forms without bond damage. Controlled curing ensures consistent handling throughout winding and downstream processing.

Quality Control For Fiber Ribbon And Flexible Flat Cable Output

Maintaining the integrity of each flat ribbon cable is a meticulous process. It involves checking the cable’s flexibility and its readiness for subsequent splicing operations. During production, operators assess the fiber count, color sequence, and precise positioning of each fiber. They also evaluate the cable’s winding condition, ensuring its optimal state for assembly.

Regular inspections are critical in identifying any defects in the coating, uneven tension, or misplaced bonds. These issues, if left unaddressed, could compromise the cable’s performance in subsequent stages of production.

Inspection Of Bond Spacing, Ribbon Width, And Thickness

Bond spacing remains a critical parameter, requiring adherence to a specific design range. This spacing is essential for the cable’s flexibility, ensuring that the fibers remain aligned within their designated subunits during bending.

Quality checks are performed to confirm that each bond correctly connects adjacent subunits. This attention to detail ensures that the ribbon lays flat, facilitating smooth mass fusion splicing processes.

Inspection Point Items Checked Process Value
Fiber identification Fiber count, color sequence, and position Helps ensure accurate splicing and maintenance
Intermittent bond arrangement Bond placement, separation distance, and subunit joining Maintains flexibility and fiber organization
Ribbon geometry Dimensional width, thickness, and flatness Ensures the ribbon works with downstream handling and splicing tools
Finished surface quality UV cure state, coating coverage, and defects Protects the ribbon against damage during take-up

Optical And Mechanical Performance Testing

Mechanical testing focuses on bond separation, cohesive strength, elongation, and handling behavior. These evaluations are essential to confirm that the manufacturing process controls are consistent across similar designs of flat cables.

Optical testing includes evaluations after bonding and curing. It ensures that the core, cladding, primary coating, secondary coating, and color layer are adequately protected throughout the manufacturing process.

Optical attenuation checks and handling evaluations are integral to routine inspections. The quality of winding is also scrutinized to ensure that the finished flat ribbon cable is in a controlled condition for assembly.

Production Automation, Efficiency, And Precision Winding

The essence of efficient ribbon production on a unified production line. Each stage, from fiber payoff to inspection and take-up, must harmonize seamlessly. This synchronization ensures the preservation of fiber geometry and facilitates consistent output, critical for high-speed data transmission cables.

Production Line Synchronization And Process Data Monitoring

Automated control systems synchronize payoff speed, fiber tension, resin delivery, bond placement, UV curing, cooling, and take-up. Adjustments are made in real time to maintain ribbon stability when speed variations occur at any station.

Manufacturing data records capture fiber color sequences, bond intervals, cure settings, ribbon dimensions, and winding status. This detailed history allows operators to track the production of each custom ribbon cable.

  • Stable payoff tension helps prevent fiber stretch and looseness.
  • Controlled bond timing maintains regular intervals between bond points.
  • Dimension monitoring identifies width and thickness variations quickly.
  • Winding data facilitates lot tracking and downstream handling.

Preparing Wound Ribbon For Downstream Cable Manufacturing

A precision cable winder helps ensure the ribbon is wound onto a spool with uniform tension and controlled movement. This method prevents edge crushing, layer crossing, and sudden pulls during subsequent cable processing.

Finished ribbon structures may be stacked, rolled, or loaded into central tube and loose tube designs. These configurations enable the creation of high-speed data transmission cables, even in areas where duct additions are impractical.

For customized ribbon products, the winding pattern must align with subsequent processes. Proper spool buildup is essential for smooth payout during stranding, tube loading, and cable assembly.

Process Area Primary Control Focus Resulting Benefit
Fiber payoff Stable tension and correct color sequence Correct ribbon positioning in downstream cable construction
Bond application Controlled bond intervals and resin quantity Flexible ribbon behavior during handling
UV cure stage Controlled lamp output and exposure time Properly cured bonds before ribbon winding
Cable winding system Uniform traverse with controlled spool tension and layering Smooth payout for central tube or loose tube loading

Ribbon Cable Applications, Splicing, And Connector Planning

Ribbon fiber plays an important role in dense links within data centers, telecom backbones, metro rings, and FTTx feeder routes. It also excels in indoor FTTH runs, 5G fronthaul, and outdoor point-to-point networks where space is at a premium.

A meticulously planned ribbon cable assembly enables crews to manage high fiber counts efficiently, without increasing bulk. Each high-speed data transmission cable must align with the site’s route, enclosure space, and future expansion plans.

Benefits Of Mass Fusion Splicing

A ribbon fusion splicer facilitates the joining of an entire ribbon in a single operation. For a 12-fiber ribbon, a matching cleaver can prepare all 12 fibers simultaneously before the automated fusion process commences.

This approach minimizes handling time and ensures consistent fiber alignment. Splice loss is reported to remain below 0.05 to 0.10 dB per fiber, contingent upon controlled preparation, cleaning, and machine settings.

Loose tube cable, on the other hand necessitates a different strategy at the splice cassette. Technicians must separate the fibers, then splice them individually, which prolongs the ribbon cable assembly process.

Dense Link Connection Planning

Multi-fiber connections commonly use MPO or MTP trunks, harnesses, fanout cables, and cassette modules. The chosen cable connector must align with the fiber count, polarity method, connector gender, and fiber type.

Connection planning also includes transceiver requirements and the full link loss budget. A high-speed data transmission cable, when used with parallel optics, demands a clear polarity path from equipment port to patch panel.

Connection Planning Item What It Controls Typical Network Use
Number of ribbon fibers Splice capacity and cassette selection 12-fiber and 24-fiber network backbones
MPO or MTP multi-fiber connector Polarity, gender, and port compatibility Data center trunks and 5G equipment rooms
Multi-fiber harness or fanout assembly Transition from multi-fiber connections to single-fiber ports Network switch connections and patch fields
Network loss budget Allowed loss from splices, connectors, and fiber length High-speed data transmission cable routes

Shanghai Weiye OFC Equipment For Fiber Ribbon Production Lines

Shanghai Weiye OFC Equipment, commonly referred to as SHWY, specializes in machinery for the production of optical fibers and cables, serving markets in the United States and globally. Its offerings are designed to support consistent manufacturing, facilitate clear operator control, and enable seamless integration into production lines.

For initiatives requiring an intermittent bonded ribbon production line, SHWY provides equipment for each stage of ribbon handling, curing, and winding with suitable machinery.

SHWY Experience With Optical Fiber And Cable Machinery

Established in 1998, SHWY’s journey in the industry has been marked by significant milestones. By 2012, its annual turnover surpassed 200 million CNY, strengthening its position within a prominent Chinese fiber and cable conglomerate as a joint venture.

SHWY became independent in 2020, relocating to a state-of-the-art facility in central Shanghai. This move underscored its commitment to advancing equipment research, manufacturing, and process application while supporting operational stability.

Relevant SHWY Production Equipment Portfolio

The SHWY equipment portfolio includes a diverse range of equipment, including fiber draw towers, coloring machines, secondary coating lines, SZ stranding equipment, and cable sheathing lines. Notably, it also features a fiber ribbon line tailored for flat, high-count fiber formats.

For fiber ribbon manufacturing projects, a cable precision winder plays a critical role in maintaining orderly package buildup and controlled tension. This ensures safer transport and more consistent feeding into subsequent cable production stages.

The company’s extensive range further includes FTTH lines, indoor cable equipment, and OPGW fiber-in-stainless-steel-tube systems. These options enable manufacturers to integrate an intermittent bonded ribbon production line with complementary cable processes.

Conclusion

An intermittently bonded ribbon production line combines fiber alignment, controlled bonding, UV curing, inspection, and precision winding into a unified process. Each step helps preserve fiber sequence while maintaining the necessary bendability for dense cable designs. This combination is critical for the creation of high-density optical networks.

The resulting ribbon structure provides efficient mass fusion splicing and organized fiber management. It is well suited to applications involving high fiber counts, confined ducts, limited tray space, and frequent splice points. This makes it a cornerstone in many high-density ribbon cable routes.

Successful project planning goes beyond the production line. It encompasses the cable structure, closure capacity, fusion tools, test methodologies, labeling, and restoration records. These elements must align with the planned network architecture for seamless integration.

Related: Compact Fiber Unit for Telecom Carriers
         Comparing Compact Fiber Units: Features and Performance